B2B Technical Sourcing & Engineering Whitepaper
THIN KERFDIAMOND TILEDRILLS GUIDEFOR GLOBAL BUYERS
The definitive B2B guide to Thin Kerf Diamond Tile Drills: Analyzing vacuum-brazed metallurgy, dry porcelain penetration dynamics, total cost of ownership (TCO), and global procurement trends for hard ceramic substrates.
Information Gain & Technical Analysis
The Physics & Metallurgy Behind Thin Kerf Diamond Tile Drills
Global procurement managers, commercial buyers, and industrial tool specifiers increasingly encounter a major challenge: the modern tile industry's rapid evolution toward dense, large-format porcelain slabs (Porcelain Gres), Dekton, quartz, and vitreous glass tiles. Standard diamond core bits designed a decade ago struggle with heat buildup, slow linear penetration rates, and micro-fracturing along tile margins.
1. Mechanical Kerf Dynamics & Surface Contact Reduction
The term "kerf" refers to the width of the cut made by a drilling tool. Conventional diamond core drills feature a crown wall thickness of 2.2mm to 2.8mm. In contrast, Thin Kerf Diamond Tile Drills engineered by DURO utilize a ultra-narrow crown profile measuring only 1.0mm to 1.2mm.
This subtle reduction in wall geometry delivers exponential mechanical benefits. By reducing the surface contact area between the diamond matrix and the ultra-hard ceramic substrate by up to 45%, the total torque required from the power tool drops precipitously. Modern cordless 18V/20V angle grinders and high-rpm tile drills consume substantially less wattage per millimeter of hole depth. Field trials demonstrate that operators achieve up to 2.8 times more holes per battery charge while maintaining a linear cutting speed up to 60% faster than standard core bits.
2. Vacuum Brazed Bond vs Electroplated & Sintered Matrix
For decades, cheap tile drills relied on electroplating, where synthetic diamond grit is lightly held onto a steel shell via an electrodeposited nickel matrix. Electroplated tools suffer from severe thermal degradation; as temperatures exceed 250°C, the nickel layer softens, causing premature diamond pull-out and sudden tool glazing.
DURO Thin Kerf Diamond Tile Drills utilize high-vacuum furnace brazing at temperatures exceeding 1,000°C. An active nickel-chromium-titanium alloy chemically bonds and encapsulates synthetic diamond grains directly to the high-tensile steel barrel. This chemical fusion provides extraordinary diamond grain retention (up to 85% diamond exposure before pull-out occurs) and creates dedicated thermal dissipation channels between individual diamond points.
Commercial Tooling Portfolio
Engineered Product Recommendations for Procurement Teams
Select the exact specification required for your distribution inventory or direct contractor fleet.
DDC-RAPIDE M14 Thin Kerf Tile Drills
Engineered for direct mounting onto 10,000–12,000 RPM angle grinders. Features high-concentration vacuum-brazed diamond crowns with internal paraffin cooling wax (6mm–14mm) and perimeter airflow flutes for rapid dry core drilling in Grade 5 porcelain and sintered stone.
Inquire Commercial Stock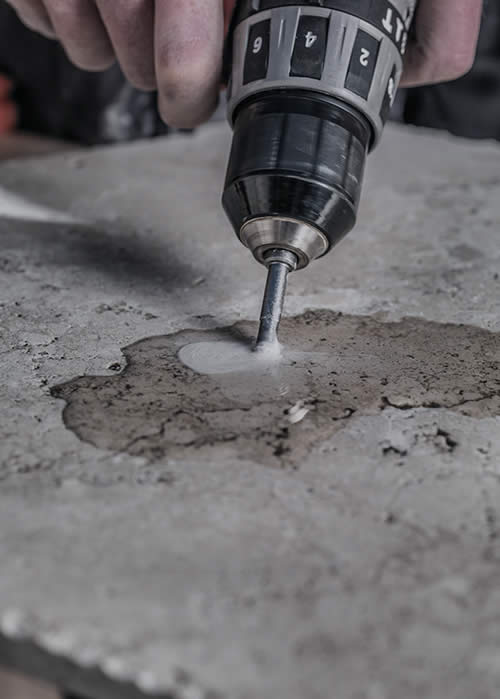 Dry Porcelain Drilling
DU-DHS Quick-Change Thin Kerf Tile Bits
Designed for cordless impact drivers and standard drill chucks (2,000–3,000 RPM). Features non-slip 1/4" hex shanks, ultra-thin wall construction, and self-cooling internal thermal phase lubricant. The primary selection for plumbers and electrical installers.
Request Wholesale PricingTechnical Performance & Specification Benchmark Matrix
Data gathered from live field testing under controlled laboratory conditions on 12mm PEI Class V Porcelain Gres slabs.
| Drill Series | Diameter Range | Shank / Fitting | Optimum Operating Speed | Cooling Method | Average Hole Speed (12mm Tile) | Expected Tool Life |
|---|---|---|---|---|---|---|
| DDC-RAPIDE M14 Thin Kerf | 5mm – 120mm | M14 Female Thread | 10,000 – 12,000 RPM | Internal Wax / Air Slots (Dry) | 4.2 Seconds | 65 – 110 Holes |
| DU-DHS Hex-Shank Series | 5mm – 35mm | 1/4" Quick-Release Hex | 2,500 – 3,500 RPM | Thermal Phase Gel / Paraffin | 8.5 Seconds | 40 – 75 Holes |
| DURO Continuous Rim Wet Tile Cores | 6mm – 150mm | 1/2" BSP / Straight Shank | 1,800 – 3,000 RPM | External Water Feed Tank | 3.1 Seconds | 150 – 240 Holes |
Market Analysis & Sourcing Intelligence
Future Global Procurement Trends for Diamond Tile Drilling Tools
Sourcing directors and commercial buyers must look beyond the initial unit cost when specifying tooling inventories for regional distribution or major construction tenders. Modern diamond tool procurement is shaped by four macro-economic and technical trends:
Trend 1: The Dominance of Sintered Stone & Ultra-Compact Surfaces
Architectural preferences have shifted rapidly toward materials like Dekton, Neolith, and 20mm outdoor porcelain pavers. These materials exhibit Mohs hardness ratings exceeding 7.5 and internal tensile stresses that cause shattering when drilled with aggressive or thick-walled tools. Thin Kerf Diamond Tile Drills eliminate thermal stress propagation, making them the mandated standard for high-end kitchen, bath, and facade installations worldwide.
Trend 2: Transition from Wet Drilling to High-Speed Dry Drilling
While wet drilling extends tool life, modern job sites prioritize clean, fast, and cordless operations. Contractors waste billable hours setting up water supply lines or cleaning slurry off finished walls. High-RPM vacuum-brazed dry thin kerf drills enable instant hole creation with zero slurry, driving massive contractor demand across Europe, North America, and Australia.
Trend 3: Total Cost of Ownership (TCO) Procurement Metrics
Commercial buyers are moving away from cheap, uncertified import bits that fail after 3 to 5 holes. Professional contractors compute cost-per-hole. A premium DURO Thin Kerf Drill delivering 80+ clean holes at 4 seconds per hole vastly outperforms low-grade tooling in labor-hour savings, making certified high-performance tools easier to sell at higher gross margins.
Trend 4: Strict Enforcement of Health & Silica Dust Regulations
Regulatory bodies such as OSHA (USA) and the HSE (UK) strictly enforce respirable crystalline silica (RCS) dust exposure limits. Advanced thin kerf tile drilling creates up to 40% less total swarf volume than thick-walled bits, allowing seamless integration with vacuum shroud extractors and site dust suppression tanks.
R&D & Metallurgical Advancement
Next-Generation Development Trends in Tile Drilling Engineering
To maintain competitive advantages in global markets, DURO's research and development engineering teams focus on three emerging technology pillars:
1. Advanced Synthetic Diamond Coatings
Integration of titanium-coated synthetic diamond monocrystals. The titanium shell acts as a sacrificial thermal barrier, preserving the underlying diamond lattice structure even under momentary dry friction spikes above 800°C.
2. Micro-Encapsulated Phase-Change Coolants
Development of high-viscosity bio-wax matrix compounds housed inside small-diameter bit shafts. Micro-channels meter the fluid release precisely as drilling torque warms the barrel, preventing waste and extending bit life by up to 35%.
3. Multi-Fit Universal Fitting Geometries
Designing combination shanks that seamlessly adapt between M14 angle grinder spindles and hex-shank quick-release cordless drills without requiring prone-to-wobble threaded adapter collars.
Enterprise Reliability & Manufacturing Power
Why Global Tool Distributors & OEMs Choose DURO Yokota
With over 20 years serving professional trades across construction, surface preparation, and industrial distribution, DURO combines field-tested application expertise with uncompromising manufacturing discipline.
All DURO diamond consumables are manufactured in audited oSa (Organization for the Safety of Abrasives) member facilities. Safety parameters under EN 13236 and EN 12413 are integrated directly into our metallurgy and quality control protocols — ensuring zero segment detachment risks on high-speed power tools.
Our operations run under a rigorous quad-ISO management structure: ISO 9001 (Quality), ISO 14001 (Environmental), ISO 45001 (Occupational Health & Safety), and ISO 27001 (Information Security).
 Precision Engineering
Material Matched Bonds
Specifically calibrated diamond matrix formulas for soft ceramic, hard vitreous tile, Grade 5 porcelain, and quartz slabs.
In-Store Merchandising
Custom display stands, point-of-sale display boards, and packaging designed to maximize stock turn on trade counter shelves.
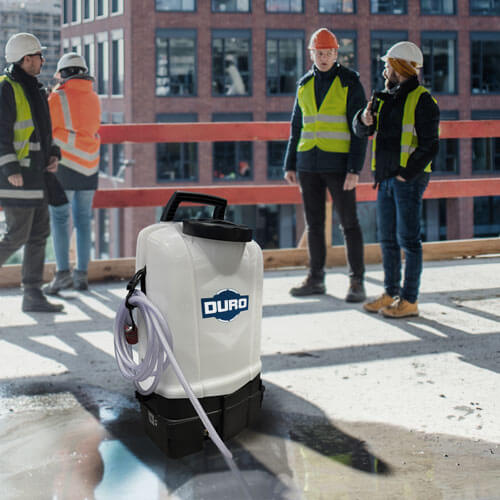 Site Compliant Safety
Proprietary Technology Highlight
DDC-RAPIDE: Benchmark Vacuum Brazed Technology
The engineering breakthroughs established in our flagship DDC-RAPIDE heavy-duty core drill range directly inform our Thin Kerf Diamond Tile Drill chemistry. By eliminating conventional laser-welded segments in favor of a continuous brazed diamond matrix, tool failure is virtually eradicated.
- Up to 60% faster linear material penetration compared to standard segmented drills
- Eliminates segment detachment hazards in thin, brittle porcelain and composite slabs
- Maintains identical hole diameter from the 1st cut to the end of tool life
- Dramatically reduced vibration and machine load during hand-held dry drilling
- Proven across porcelain, granite, marble, glass, engineering brick, and tile
Complete Tooling Solutions
Explore DURO's Full Cross-Referenced Catalog
Build a complete, single-source procurement package across all hard material cutting and drilling disciplines.
Thin Kerf Diamond Tile Drills
Dry drilling through the hardest Grade 5 porcelain and quartz.
View range Diamond Holesaws
Fast, clean holes in tile, masonry, and plastics.
View range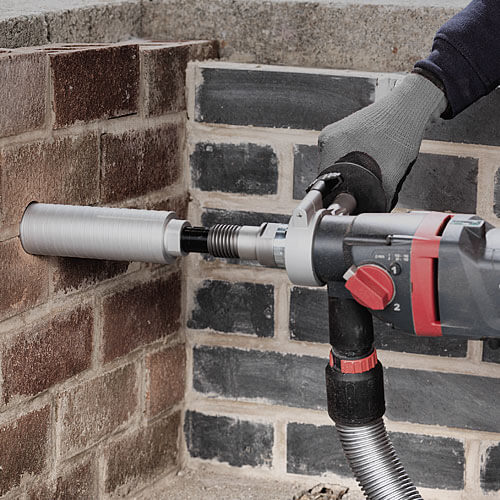
Vacuum Brazed Core Drills
DDC-RAPIDE high-speed core bits for construction.
View range Dust Suppression Tanks
10L–60L site water tanks including battery powered units.
View rangeEngineering & Sourcing FAQ
Frequently Asked Questions by Global Tool Procurement Teams
Expert answers addressing intent, application limits, thermal physics, and wholesale logistics.
Thin Kerf Diamond Tile Drills feature a significantly reduced crown wall thickness (typically 1.0mm to 1.2mm compared to standard 2.5mm bits). This reduces the contact surface area during drilling by up to 45%, lowering friction, minimizing heat generation, and dramatically reducing torque requirement on cordless power tools. The result is up to 3x faster drilling speeds, zero substrate cracking or edge-chipping, and double the holes drilled per battery charge.
Electroplated drill bits feature diamond grit held loosely on the surface by a thin nickel layer, which rapidly wears off under high friction and heat. Vacuum Brazed Thin Kerf Drills utilize high-temperature vacuum furnaces (over 1000°C) where active nickel-titanium alloy bonds fused directly to the synthetic diamond crystals and steel body. This creates a chemical and mechanical bond that retains diamonds up to 85% worn down, allowing high RPM dry drilling on hard materials without segment loss or glazing.
Yes. DURO Thin Kerf Diamond Tile Drills in small diameters (5mm to 14mm) are engineered with internal thermal-phase change cooling wax or vegetable-based paraffin cores. As drilling heat builds, the internal wax melts, lubricating the diamond cutting edge from the inside out and absorbing excess heat. For larger diameters (15mm to 120mm), high-density vacuum brazed diamond crowns with lateral cooling slots purge dust and dissipate heat rapidly during dry high-RPM operation on angle grinders.
For optimal cutting speed and diamond life, M14 Thin Kerf Diamond Tile Drills should be operated between 10,000 RPM and 12,000 RPM. High rotational speed creates micro-impact fracturing of the porcelain surface while preventing thermal shock accumulation. Operators should use a slight orbital or oscillating motion during drilling to facilitate air cooling and swarf removal.
The primary causes of tool glazing are applying excessive axial down-force, running power tools below recommended RPMs, or failing to use an orbital rocking motion during dry drilling. When an operator pushes too hard without rocking the tool, swarf becomes trapped inside the kerf, grinding against the body and building heat above 600°C. Allowing the diamond crown to breathe and clear dust every few seconds maintains free-cutting efficiency.
DURO provides full commercial support, including dual UK warehouse stock availability, next-day despatch, custom packaging options, branded retail merchandising units, and complete technical compliance documentation (oSa safety compliance, EN 13236, and ISO 9001, 14001, 45001, 27001 certifications). Direct OEM and wholesale inquiry support is available via our Live Chat portal.
Yes. DURO works closely with major industrial resellers, international buying groups, and equipment hire fleets. We offer tailored core drill lengths, specialized shank fittings (such as 1/2" BSP, SDS-Plus adapters, or custom quick-change hex designs), as well as customized retail point-of-sale display solutions for regional distributors.
Global Wholesale & OEM Sourcing
Partner with DURO Yokota for Premium Diamond Tooling Supply
Connect directly with our engineering sales specialists to evaluate pricing, request sample test packs, or discuss custom distributor display options for your region.
Dedicated technical response within 24 business hours. Dual-warehouse order despatch supported.