Engineered for extreme material hardness, tight dimensional tolerances, and high-speed linear processing. Fully customizable for Japanese and international CNC sawing systems.
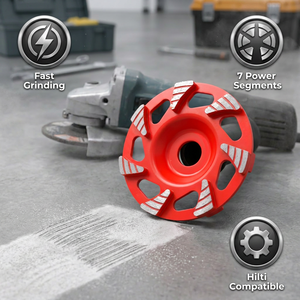
Heavy-duty concrete floor surface prep cup wheel with Hilti-compatible arbor. High-diamond matrix concentration engineered for aggressive coating removal.
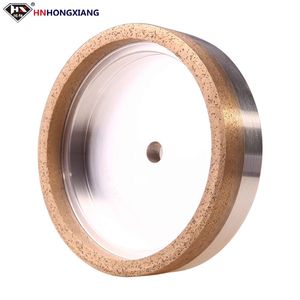
Precision-balanced sintered glass grinding wheel designed for high-speed edge beveling, bevel polishing, and zero-chip finishing on technical glass.
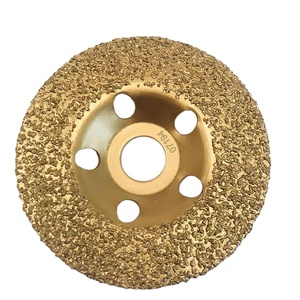
115/125/180mm abrasive cup wheel utilizing direct vacuum-brazed tungsten carbide grit for non-loading removal of heavy epoxy, polyurethane, and mastic.
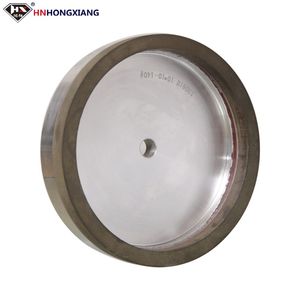
Industrial-grade metal-bonded diamond cup wheel optimized for automated double-edger machines, ensuring long wheel life and micro-smooth arris edges.
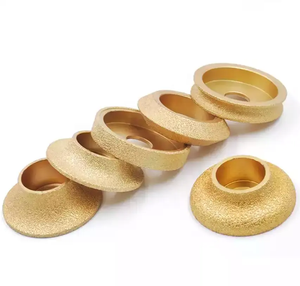
Compact profile cup wheel engineered for detail work, corner profiling, and internal radius grinding on granite, marble, and engineered quartz slabs.
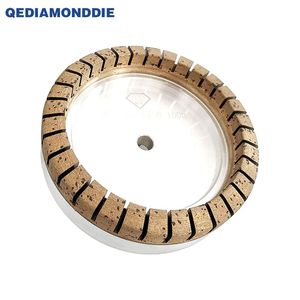
Continuous rim full-toothed segment design for rapid stock removal on architectural curtain wall glass, reducing vibration and rim thermal fracturing.
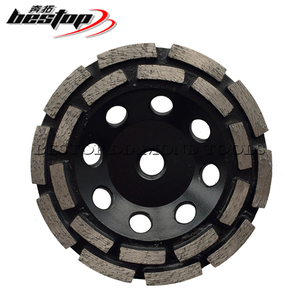
Heavy-duty double row segment layout with silver brazed joints for maximum structural security. Fully custom OEM logo, arbor size, and bond hardness available.
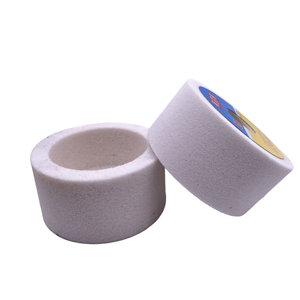
Vitrified white aluminum oxide cup wheel designed for toolroom tool grinding, alloy steel sharpening, and precision surface finishing without thermal damage.
As semiconductor substrates shift toward ultra-wide bandgap materials like Silicon Carbide (SiC) and Gallium Nitride (GaN), traditional blade slicing methods fail to meet the strict total thickness variation (TTV) and surface roughness ($Ra$) required by modern fabrication facilities. Diamond wire sawing—specifically utilizing high-tensile carbon steel cores plated with monocrystalline synthetic micro-diamonds—has emerged as the definitive global standard.
Our OEM/ODM manufacturing facilities produce both continuous endless diamond wire loops and long spooled multi-wire saw inputs. By controlling the nickel bath chemical kinetics, diamond particle orientation, and core wire thermal treatment, we eliminate common failure modes such as wire bow tension decay, diamond pull-out, and localized core stripping.
| Wire Technology Type | Primary Substrates | Grit Range (µm) | Core Wire Material | Max Linear Speed | Key Advantage |
|---|---|---|---|---|---|
| Electroplated Diamond Wire | SiC Ingot, Sapphire, Monocrystalline Silicon | 6 µm – 45 µm | High-Carbon Steel (SWRS) | 80 m/s | Ultra-thin kerf width (<0.12mm), minimal material yield loss. |
| Resin-Bonded Diamond Wire | Quartz Glass, Technical Ceramics, Optical Lens blanks | 15 µm – 60 µm | Stainless / Spring Steel Wire | 50 m/s | Self-sharpening matrix elasticity; prevents micro-cracking in brittle glass. |
| Vacuum Brazed Diamond Loop | Carbon Fiber, Ferrite, Concrete, Tire Cut Sections | 46 # – 120 # | Pre-stressed Alloy Core Wire | 35 m/s | Extremely high diamond retention; cuts composite steel-concrete structures seamlessly. |
| Heavy Construction Wire | Reinforced Concrete Pier Cutting, Subsea Steel Structures | Segment Sintered (D602) | Multi-strand Galvanized Cable | 25 m/s | High tensile pulling load resilience; replaceable sintered diamond beads. |
Osaka and the broader Kansai economic corridor (including Sakai, Higashiosaka, and Kadoma) represent one of the world's most concentrated clusters for semiconductor equipment, precision optical component manufacturing, and heavy civil marine engineering.
Achieve Total Thickness Variation (TTV) under 5µm on 200mm wafers with custom-engineered diamond spatial density distribution.
Proprietary seamless micro-laser weld splicing guarantees joint tensile strength equal to 95%+ of the parent wire body, preventing joint breakage at speeds exceeding 60 m/s.
As Japanese manufacturers accelerate compliance with Green Transformation (GX) initiatives and automated smart factory standards, diamond wire technology is evolving rapidly.
Kansai-based semiconductor foundries are completely phasing out silicon carbide slurry slicing in favor of electroplated fixed-diamond wire. Fixed wire sawing yields 40% faster cutting speeds, eliminates hazardous slurry disposal costs, and dramatically cuts power consumption per sliced wafer.
Strict compliance with Japanese Ministry of Health, Labour and Welfare (MHLW) guidelines for respirable crystalline silica dust has driven high demand for integrated wet-cut diamond wire extraction systems. Water feed combined with inline centrifugal filtration units protects operator safety while extending wire life.
R&D efforts in Osaka are demanding core wire diameters pushing below 0.08mm for rare earth magnetic materials and expensive single-crystal substrates, where raw material cost recovery outweighs tool consumption expenses.
Backed by over two decades of metallurgical research and audited under rigorous international standards, our diamond consumables deliver uncompromised batch-to-batch consistency. Every production batch undergoes automated optical diamond distribution scans, tensile load break testing, and dynamic balance calibration.
We specialize in contract private-label manufacturing (OEM) and custom wire design (ODM) tailored to specific OEM machine kinematics, coolant viscosities, and feed speeds.
Detailed technical and commercial responses to ensure seamless integration into your local factory workflows.
For standard spooled electroplated diamond wire, orders ship within 5 to 7 business days. Custom-length laser-spliced endless diamond wire loops optimized for specialized CNC machines typically ship within 10 to 14 business days. Expedited air freight directly to Kansai International Airport (KIX) or direct sea freight to Osaka/Kobe ports is routinely managed with full customs clearance support.
Silicon Carbide is extremely hard (9.5 Mohs). When cutting at linear speeds up to 80 m/s, lower quality steel wire suffers from tension loss, resulting in "wire bow" which causes parabolic wafer taper and excessive Total Thickness Variation (TTV). We utilize ultra-high tensile carbon steel core wire (3,800 MPa rating) that maintains constant axial tension under high feed pressure, yielding flat wafer surfaces and zero micro-cracking.
Yes. All diamond abrasive products are manufactured in compliance with JIS B4131 (Diamond/CBN Abrasive Products) and audited under European safety standard EN 13236. Manufacturing plants hold active oSa® (Organization for the Safety of Abrasives) accreditation, providing Osaka facility managers with complete audit compliance for industrial safety inspections.
Electroplated wire features a single, densely packed layer of micro-diamonds anchored by a nickel plating matrix. It provides maximum cutting aggressiveness and the absolute thinnest possible kerf width. Resin-bonded diamond wire features a multi-layer resin matrix that slowly erodes to expose fresh diamond edges. Resin-bonded wire is preferred for brittle optical glasses and quartz crystal, as the resin acts as a shock absorber to prevent edge chipping.
Absolutely. We manufacture continuous wire loops compatible with major Japanese and international wire saw brands (including Takatori, Meyer Burger, Komatsu, and NTC). Our joint splicing utilizes sub-millimeter laser butt welding, followed by diamond re-plating across the splice zone so that the joint diameter matches the rest of the wire within a 2µm tolerance.
We provide comprehensive engineering support to pair our wire matrix with your coolant infrastructure. Generally, low-viscosity synthetic water-soluble coolants with rust inhibitors and surface-active wetting agents are recommended for semiconductor slicing to flush micro-swarf out of the kerf rapidly.
Consult directly with our diamond abrasive engineering team. We provide sample testing, wire matrix formulation matching, and factory direct pricing for Osaka and global manufacturers.
Send an Inquiry