Engineered for extreme material removal rates, heavy-duty floor restoration, precision glass polishing, and aggressive masonry milling.
Building high-yield industrial step drills, vacuum brazed core tools, and surface prep consumables requires rigorous quality control, metallurgically optimized bonding, and strict compliance with international safety directives.
Every diamond blade, step drill bit, and grinding cup wheel is manufactured under strict oSa (Organization for the Safety of Abrasives) guidelines. We guarantee compliance with EN 13236 and EN 12413 standards to eliminate segment detachment and structural failure during high-RPM operations.
Our global production hubs and data infrastructure are fully certified to ISO 9001:2015 (Quality Management), ISO 14001:2015 (Environmental Standards), ISO 45001:2018 (Occupational Health & Safety), and ISO 27001 (Information Security).
Utilizing high-vacuum furnace brazing, diamonds and tungsten carbide grains are chemically bonded directly to the steel body. This delivers up to 60% faster cut rates compared to conventional sintered tooling, eliminating segment loss entirely.
In B2B industrial procurement, matching abrasive diamond matrix hardness and step drill coating geometry to target substrate compressive strength is vital for minimizing total cost per hole or square meter.
Whether drilling through sheet metal, deburring structural steel, removing high-build epoxy coatings, or profiling architectural glass, selecting an under-specified or over-hardened tool results in glaze-over, premature segment loss, or excessive thermal deformation. The selection matrix below details metallurgical compatibility across our key tool categories:
| Tool Category | Bond / Coating Metallurgy | Target Substrate | Operational Speed (RPM / Surface Feed) | Primary Technical Advantage |
|---|---|---|---|---|
| Industrial HSS / Co Step Drills | TiAlN / TiN Multi-Layer PVD Coating | Stainless Steel, Alloy Sheet Metal, Structural Aluminum | 400 – 1,200 RPM (Lubricated) | Self-centering split point; burr-free multi-diameter hole expansion without bit changing. |
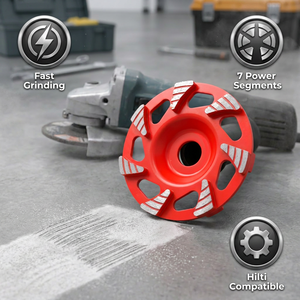
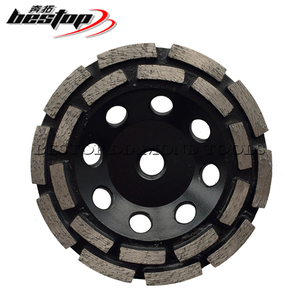
| Aggressive Floor Prep Cup Wheels | Co-Cu Soft Matrix + 7/12 Segment Blocks | Green Concrete, Cured Reinforced Concrete, Terrazzo | 8,500 – 11,000 RPM (Dry/Wet) | High diamond concentration (30/40 Grit) for fast stock removal prior to epoxy coating. |
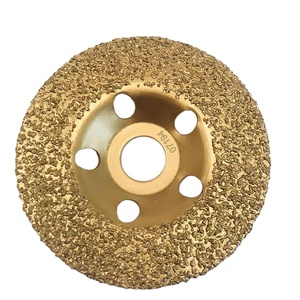
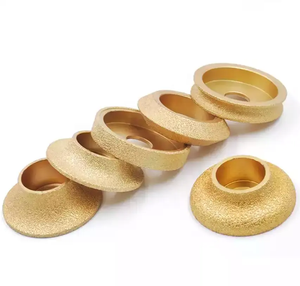
| Vacuum Brazed Carbide Cup Wheels | High-Temperature Nickel-Chromium Braze Matrix | Epoxy Resins, Polyurethane, Elastomeric Mastics, Paint | 6,000 – 10,000 RPM (Dry) | Coarse tungsten carbide grit prevents loading and clogging on sticky, thermosoftening coatings. |
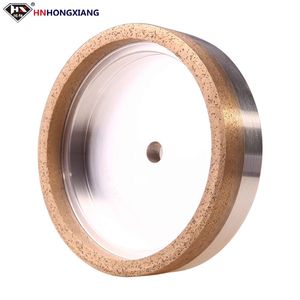
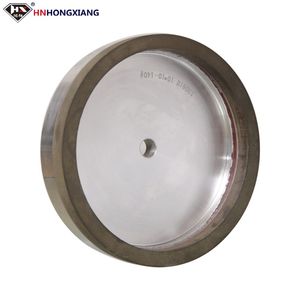
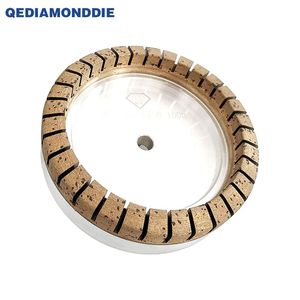
| Architectural Glass Cup Wheels | Fine-Grained Metal-Sintered Bond (180–320 Grit) | Low-E Glass, Laminated Safety Glass, Double-Sided Edgers | 2,800 – 4,500 RPM (Flood Water Cooling) | Full-toothed or continuous rim configuration preventing edge micro-chipping and thermal fracture. |
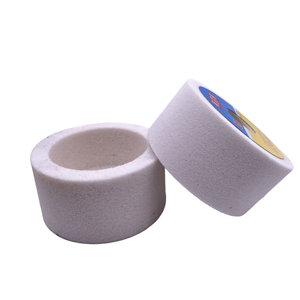
| Ceramic White Corundum Wheels | Vitrified Alumina Matrix (WA 125*63*32) | Tool Steels, Hardened Alloy Steel, Machine Parts | 35 – 45 m/s Surface Speed | High-purity self-sharpening abrasive grains for cool, burn-free tool room grinding. |
Global industrial supply chains are transitioning toward ultra-durable, multi-material tooling engineered to lower downtime and strictly comply with worker health regulations.
Regulatory authorities worldwide (including OSHA, EU-OSHA, and UK HSE) are enforcing stringent limits on airborne crystalline silica (RCS). Modern procurement managers are prioritizing on-tool extraction shrouds and battery-powered dust suppression water tanks (10L–60L capacity) integrated directly into diamond core drilling and grinding systems.
Traditional laser-welded or silver-soldered segment bits face risk of segment detachment when striking steel rebar or composite joints. The industry trend is rapidly shifting toward single-layer vacuum brazed tools (such as our DDC-RAPIDE series). By chemically fusing diamonds to the barrel wall, tool life increases while total risk of site accidents drops to near zero.
B2B buyers increasingly demand direct manufacturer customization—spanning specialized shank geometries (SDS-Max, Hilti-compatible slotted arbors, M14, 5/8"-11) to custom color-coded bond matrixes. Furthermore, buyers require full ISO certification documentation, EN safety compliance certificates, and batch-level quality control tracking.
Advanced engineering breakthroughs in physical vapor deposition (PVD) coatings, diamond grit micro-friability control, and automated laser sintering.
Next-generation step drill bits incorporate Titanium Aluminum Nitride (TiAlN) nanostructured coatings. This layer creates a thermal barrier capable of withstanding operating temperatures up to 900°C, drastically extending tool hardness when drilling dry through tough austenitic stainless steel grades (304/316).
Modern continuous-rim and segment cup wheels utilize high-purity synthetic diamond crystals with engineered friability. Under shear load, the diamond micro-fractures at a controlled rate, continually exposing crisp, sharp cutting edges while maintaining matrix integrity during concrete floor surface grinding.
Vibration is the leading cause of premature tool wear, spindle bearing damage, and operator fatigue. Our premium cup wheels undergo computer-controlled 3D dynamic balancing (achieving <0.2g·cm residual unbalance) alongside laser-cut noise-damping expansion slots.
Direct answers from our engineering desk regarding tool performance, field safety, and custom manufacturing capability.
In extensive field trials, vacuum brazed core drills (such as the DDC-RAPIDE system) remove material up to 60% faster than standard segmented core bits. Because diamonds are chemically bonded using a high-temperature nickel matrix, the entire exposed surface maintains continuous contact with the substrate. This eliminates segment shear risk, reduces machine motor strain, decreases operator fatigue, and yields consistent penetration rates from the first hole to the last.
Controlling respirable crystalline silica (RCS) requires integrated engineering controls. DURO supplies specialized dry-cutting systems optimized for direct extraction shrouds connected to M-Class or H-Class industrial vacuums. Additionally, we provide 10L to 60L dust suppression water tanks (including 20L and 60L battery-powered site bowsers) that deliver continuous pressurized water flow to the cut line—reducing airborne respirable dust concentrations by over 95%.
Yes. All DURO diamond tooling is manufactured in oSa-member facilities, meaning production processes undergo rigorous annual audits to verify compliance with European Safety Standards EN 13236 (for superabrasives) and EN 12413 (for bonded abrasives). Furthermore, corporate operations are certified under quadruplicate ISO standards: ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, and ISO 27001.
Selection follows an inverse rule: Soft materials require hard bonds; hard materials require soft bonds. Soft, abrasive substrates (such as green concrete, asphalt, or soft rain-damaged slab) quickly wear away matrix material, so a tough, tungsten-reinforced metal bond is required. Conversely, hard, non-abrasive substrates (such as dense engineering brick, granite, or cured power-troweled concrete) require a softer cobalt/copper bond matrix that breaks down easily to continually expose fresh diamond points.
As a global direct-factory exporter, we support comprehensive OEM/ODM customization. This includes custom laser-etched branding, custom step drill diameter increments, specialized arbor configurations (including Hilti, SDS-Max, 22.23mm, M14, 5/8"-11, and keyway slots), tailored diamond grit blend matrixes, and fully customized retail point-of-sale packaging for wholesale distribution channels.
Whether you require high-volume OEM step drill bit manufacturing, custom diamond grinding cup wheel production, or factory-direct wholesale pricing for hire fleet operations, our engineering team provides full technical assistance and fast international dispatch.
ISO 9001 · 14001 · 45001 · 27001 Accredited Factory | Guaranteed Fast OEM Sample Response