Explore our ISO 9001 and oSa certified high-performance grinding wheels, vacuum-brazed cup tools, and architectural grinding media built for extreme durability and ultra-fast stock removal.
From jobsite-proven metallurgical matrices to certified safety standards, our manufacturing framework eliminates operational risk for distributors and wholesale buyers.
All diamond consumables and abrasive flap discs are produced under strict audits adhering to European EN 13236 and EN 12413 safety norms, preventing wheel burst and segment detachment during heavy operation.
Our state-of-the-art facilities hold official accreditation for ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, and ISO 27001, ensuring total traceable quality from raw alloy powders to finished packing.
We offer four distinct matrix hardness performance levels. Specifiers match aggregate hardness (soft, medium, hard, ultra-hard) directly to workpiece characteristics to maximize G-ratio performance.
In modern industrial manufacturing, surface engineering, and heavy metal fabrication, the abrasive tool selection process directly impacts total cost of operation (TCO), workplace safety, and throughput speed. As a premier flap disc manufacturer and exporter, our engineering philosophy bridges advanced metallurgical powder synthesis, automated grain orientation technology, and strict compliance with European safety guidelines. This technical document provides procurement managers, industrial distributors, and structural engineering specialists with key insights into high-yield abrasive consumables, diamond cup wheel matrix mechanics, and upcoming procurement benchmarks.
Traditional abrasive flap discs relied heavily on standard aluminum oxide grains, which suffered from rapid surface glazing, excessive friction heat, and micro-welding when applied to high-tensile metals. Modern industrial manufacturing demands next-generation abrasive grains engineered for aggressive stock removal and prolonged operational longevity.
| Grain / Bond Architecture | Primary Substrate Application | Self-Sharpening Mechanism | Relative G-Ratio (Material Removed / Tool Wear) |
|---|---|---|---|
| Ceramic SG Grain (Resinoid Bond) | Stainless Steel, Inconel, Hardened Alloy | Nano-Crystalline Micro-Cleavage | 9.5 / 10 |
| Zirconia Alumina (Flap Disc) | Structural Carbon Steel, Cast Iron | Micro-Fracturing under High Load | 7.8 / 10 |
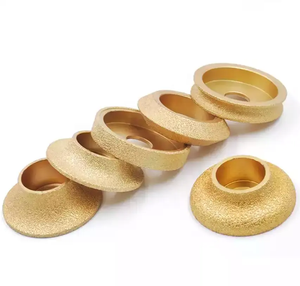
| Vacuum Brazed Diamond / Carbide | Epoxy Coatings, Thermoplastic, Green Concrete | Open-Structure Chip Clearance Clearance | 9.8 / 10 |
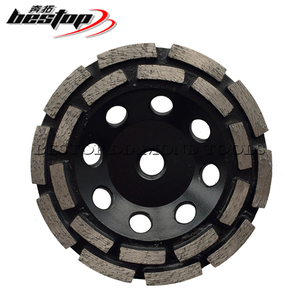
| Sintered Segmented Diamond Cup | Reinforced Concrete, Granite, Architectural Glass | Controlled Matrix Erosion & Diamond Release | 9.2 / 10 |
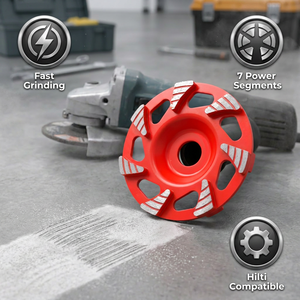
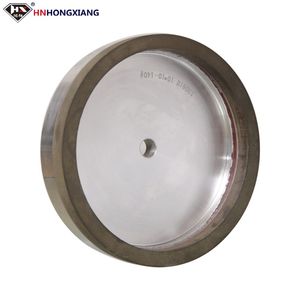
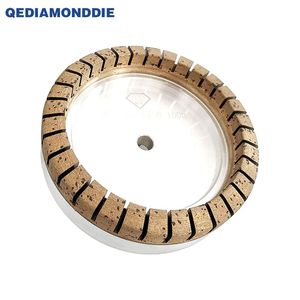
When selecting surface preparation tooling such as the SUMO Aggressive 5 Inch 125mm 7 Segments Diamond Grinding Cup Wheel or specialized Glass Diamond Cup Wheels, matching the metallic bond matrix to substrate abrasiveness is paramount to prevent glazing or premature wear.
The sintered diamond segment is a composite of synthetic diamond crystals embedded inside a powder metallurgy matrix composed of cobalt, iron, copper, tungsten carbide, and nickel. During heavy grinding on tough aggregates (such as reinforced concrete or architectural float glass), the metallic bond must wear away at a rate proportional to the diamond crystal breakdown:
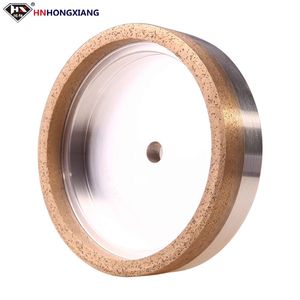
For high-precision architectural glass processing, full-toothed and sintered cup wheels utilize micro-mesh diamonds (mesh sizes #120 to #400) to deliver chip-free edge profiles on double-sided straight edge processing machines. Dynamic balancing to tolerances below 0.02 grams ensures chatter-free operation and extends machine spindle seal lifespan.
Industrial B2B buyers, OEM private label brand owners, and international stocking distributors face evolving regulatory standards, shifting supply chain paradigms, and technological breakthroughs. Procurement teams are moving away from evaluating consumables solely on unit purchase price, shifting toward Total Cost of Removal per Square Meter (TCR/m²) metrics.
With the rapid expansion of robotic welding arms and automated gantry grinding stations in automotive and structural steel manufacturing, flap discs and grinding wheels must maintain strict dimensional tolerances, predictable wear rates, and zero out-of-round variance to prevent automated cell shutdown.
Regulators globally (OSHA silica standards in the US, EU Directive 2017/2398) strictly enforce dust limits. Modern abrasive cup wheels feature engineered air-venting segments, integrated shroud dust shrouds, and wet-feed channels compatible with portable 10L to 60L dust suppression water bowsers.
Furthermore, sustainability initiatives are driving green manufacturing in the abrasive sector. Leading manufacturers are transitioning toward phenol-free resin binder systems, VOC-free curing ovens, fully recyclable fiberglass backing plates (Trimming Flap Discs), and sustainable export packaging programs compliant with ISO 14001 guidelines.
Operating high-speed abrasive tooling at peripheral speeds up to 80 m/s presents inherent safety considerations. A disc rupture at 12,000 RPM can result in catastrophic equipment damage and operator injury. As a certified oSa member factory, our manufacturing operations enforce stringent safety verification protocols across every production batch:
For international buyers seeking private labelling OEM services, we offer customized fiberglass backing layer counts (7+1 or 8+1 structure), custom printed labels, specialized arbor hole sizes (such as Hilti snap-on or standard 22.23mm / 5/8"-11 threads), and customized grain blends tailored to specific local market demands.
Answers to common technical, compliance, and procurement inquiries from commercial buyers, specifiers, and distribution partners.
Type 27 (Flat Shape) flap discs are designed primarily for flat surface finishing, smooth blending, and surface leveling at low grinding angles between 0° and 15°. Type 29 (Conical / Angle Shape) flap discs feature a built-in 15° to 25° angle angle, enabling maximum surface contact for aggressive stock removal, heavy weld seam blending, and edge beveling.
oSa (Organization for the Safety of Abrasives) certification guarantees that the manufacturing plant undergoes strict independent safety audits against European standards EN 13236 (for superabrasives/diamond tools) and EN 12413 (for bonded abrasives). For distributors and employers, stocking oSa-marked tooling provides verifiable legal and safety compliance, mitigating product liability risks and ensuring maximum workplace safety.
Selection depends on the compressive strength and abrasiveness of the concrete substrate. Soft, green, or highly abrasive concrete requires a Hard Metal Bond matrix to prevent rapid wheel erosion. Hard cured concrete (over 40 MPa / 5000 PSI) or dense aggregate requires a Soft Metal Bond matrix so that dulled diamonds shed easily, continually exposing sharp diamond edges.
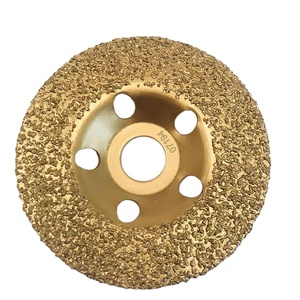
Loading occurs when soft or sticky materials (epoxy resin, urethane coatings, elastomeric paint, thermoplastic road markings) melt under grinding heat and fill the space between abrasive grains. To solve this, replace standard resin flap discs with Vacuum Brazed Tungsten Carbide Cup Wheels or open-segment PCD (Polycrystalline Diamond) cup wheels, which feature large chip clearance channels to prevent loading.
Yes. As a global exporter and manufacturer, we support complete OEM/ODM solutions including custom fiberglass backing plate artwork, laser-etched metal arbors, customized color boxes, barcode integration, and display-ready point-of-sale counter packaging designed to meet specific regional distributor requirements.
Whether you need factory-direct OEM manufacturing, container-load wholesale pricing, or technical application matching for your region, our engineering team is ready to deliver.