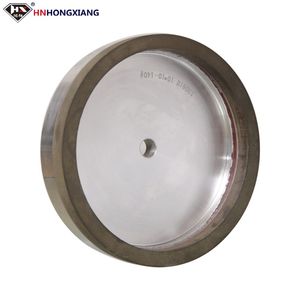
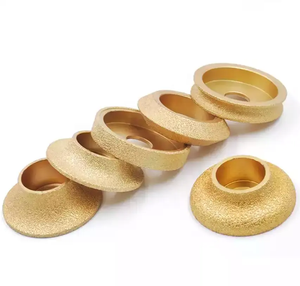
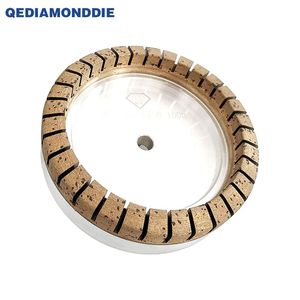
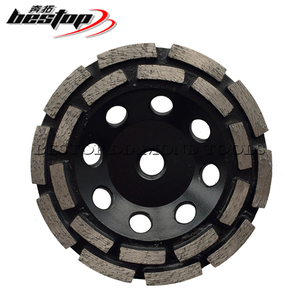
High-performance surface preparation tooling optimized for concrete grinding, glass polishing, masonry profiling, and coating removal.
Backed by 20+ years of trade expertise, certified management systems, and audited safety protocols compliant with international standards.
In high-stress industrial applications—ranging from floor scarifying and heavy concrete surface preparation to architectural glass edge polishing and tool steel re-sharpening—selecting the correct diamond or bonded abrasive cup wheel manufacturer is critical to operational efficiency, safety, and unit cost minimization. The modern abrasive market requires rigorous physical chemistry in metallurgical bonding, continuous diamond crystal matrix controls, and compliance with stringent international safety guidelines such as EN 13236 and EN 12413.
Technical Insight for Procurement Directors: The total operational cost of diamond grinding consumables is governed by the Material Removal Rate (MRR) per millimeter of segment wear rather than initial wheel acquisition cost. Sintered, laser-welded, silver-brazed, and vacuum-brazed cup wheels exhibit vastly different wear coefficients depending on substrate hardness, aggregate friability, and cooling method.
Leading cup wheel suppliers utilize four primary manufacturing technologies to anchor industrial synthetic diamond grits (or conventional alumina/silicon carbide grains) to the steel substrate:
Economical bonding process where metallic powders (Cobalt, Iron, Copper, Bronze) and synthetic diamond grits are compressed under high pressure and baked. Ideal for general-purpose masonry grinding and standard glass processing cup wheels where thermal shock is low.
Advanced high-vacuum furnace process creating a direct chemical bond between nickel-chromium alloy matrix and diamond particles. Exposes up to 70% of the diamond grit for ultra-aggressive material removal, making it unmatched for epoxy, mastic, and soft stone profiling.
Silver-solder braze applied between pre-formed diamond segments and heavy-duty carbon steel cores. Provides exceptional mechanical shock absorption under heavy angle-grinder side loads and concrete leveling operations.
To assist industrial buyers, plant managers, and tool distributors in sourcing certified cup wheels, the evaluation matrix below categorizes key technical performance indicators based on real-world application testing and auditing data:
| Bond Type | Target Substrate | Diamond Concentration | Structural Weld Strength | Optimal Operating RPM | Key Advantage |
|---|---|---|---|---|---|
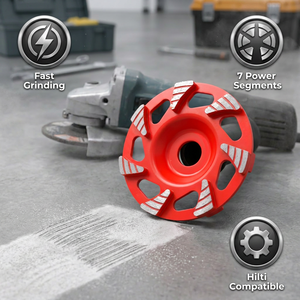
| SUMO 7-Segment Heavy Bond | Green Concrete, Rain-Damaged Slab | High (H-Grade Diamond) | Silver Brazed (>120 Nm) | 8,500 – 11,000 RPM | Aggressive rapid leveling, Hilti footprint compatible |
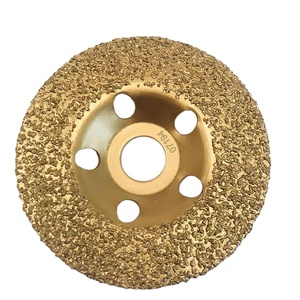
| Vacuum Brazed Carbide | Epoxy, Paint, Mastic, Tar | Direct Alloy Matrix | Fused Vacuum Bond | 6,000 – 12,000 RPM | Zero segment clogging; strips sticky coatings instantly |
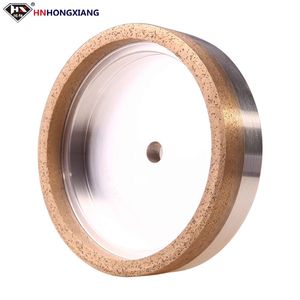
| Full-Toothed Sintered Glass | Architectural & Automotive Glass | Ultra-Fine Micron Grit | Sintered Matrix | 3,000 – 5,500 RPM | Chip-free smooth edge finish on CNC machines |
| Double Row Segmented | Cured Reinforced Concrete, Granite | Medium-High (M-Grade) | High Frequency Silver Weld | 10,000 – 12,200 RPM | Balanced long service life and cost per square meter |
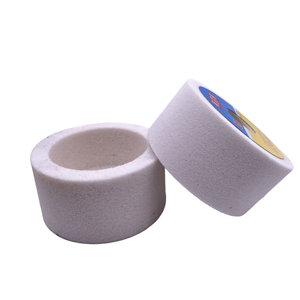
| White Corundum Ceramic (WA) | HSS Steel, Hardened Tooling | Vitrified Bond (Non-Diamond) | Monolithic Vitrified | 3,000 – 4,500 RPM | Burr-free tool sharpening without thermal burning |
A critical consideration often overlooked in procurement is matching matrix hardness inversely to substrate hardness. Grinding hard, non-abrasive substrates (such as quartz-heavy cured concrete or engineering brick) requires a soft metallic bond that sheds worn diamonds quickly, continually exposing sharp grit. Conversely, grinding abrasive materials (soft green concrete, asphalt, screed) requires a tough, wear-resistant hard bond to prevent premature diamond loss.
Furthermore, managing Respirable Crystalline Silica (RCS) dust is an imperative standard across modern worksites. Premium cup wheel manufacturers design air-flow optimized segment geometry (such as spiral cooling holes and turbo slots) that interface seamlessly with dust shrouds and high-efficiency particulate air (HEPA) vacuum extraction systems, ensuring compliance with OSHA Table 1 and European dust containment directives.
Key technological innovations reshaping surface preparation, tooling ergonomics, and B2B supplier selection over the next decade.
Global environmental regulations and supply volatility are accelerating the adoption of nickel-iron-titanium alloy matrices. These eco-friendly formulations eliminate toxic cobalt dust during manufacturing while maintaining structural segment integrity under high friction.
Next-generation automated balancing machinery ensures each cup wheel core achieves dynamic unbalance ratings below 0.05 g.mm. This dramatically reduces angle grinder vibration, minimizing operator fatigue (Vibration White Finger syndrome) and extending motor spindle bearing life.
Standardizing keyhole arbor designs, M14/5/8-11 integrated thread flanges, and universal quick-release interfaces allows single cup wheel SKUs to operate seamlessly across Hilti, Makita, Bosch, Dewalt, and Metabo grinding equipment.
Expert answers from senior application engineers to streamline your tooling specification and wholesale sourcing process.
Industrial buyers should ensure manufacturers comply with EN 13236 (Safety requirements for superabrasive products) and hold oSa® (Organization for the Safety of Abrasives) auditing credentials. This guarantees that segment shear strength, rotational bursting speed, and dynamic balance limits have undergone rigorous physical destructive testing.
Traditional segmented diamond cup wheels generate intense localized heat that melts elastomeric coatings, epoxy resin, and carpet glues, leading to rapid segment loading (clogging). Vacuum brazed carbide and diamond wheels feature exposed, sharp diamond/carbide grains that slice and chip away coatings without smearing or loading the matrix.
Single row wheels feature fewer segments, yielding maximum down-force per segment for aggressive stock removal and heavy scarifying. Double row wheels offer a smoother, flatter finish with longer tool life for general concrete floor levelling. Turbo wheels provide smooth, swirl-free finishing with continuous dust evacuation along the circumference.
Yes. Custom OEM support includes customized diamond grit distribution, tailored metal bond hardness curves for regional aggregate types, customized dynamic balancing tolerances, laser-engraved branding, private label packaging, and custom arbor hub geometries.
For diamond cup wheels grinding concrete or masonry, maximum recommended peripheral speed is typically 80 m/s (equivalent to approximately 12,250 RPM for a 125mm wheel). Operating significantly above rated RPM risks thermal fatigue and segment shear, while under-speeding leads to premature diamond pull-out.
Partner with an ISO-certified supplier to upgrade your surface preparation range, optimize grinding cost per meter, or develop custom tooling solutions.