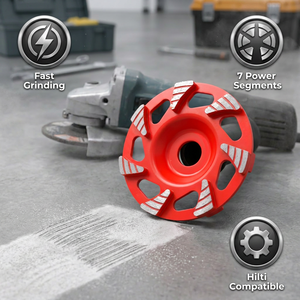
Explore our industrial-grade diamond grinding wheels, cup discs, and custom core drill accessories engineered for concrete, masonry, glass, and stone preparation.
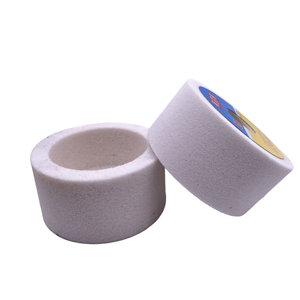
Why Tier-1 industrial buyers, hire fleets, and tooling distributors partner with our specialized core drill and abrasive wheel factories.
Our manufacturing and administrative workflows operate strictly under certified management systems: ISO 9001:2015 (Quality), ISO 14001:2015 (Environmental), ISO 45001:2018 (Occupational Health & Safety), and ISO 27001 (Information Security).
As audited members of oSa® (Organization for the Safety of Abrasives), all diamond tools are engineered and batch-tested against stringent international safety parameters mandated by EN 13236 and EN 12413 standards.
We engineer custom matrix bonds specifically balanced against substrate hardness—ranging from ultra-hard cobalt-tungsten bonds for soft abrasive asphalt, to soft free-cutting bronze matrices for heavily reinforced granite.
Our flagship DDC-RAPIDE vacuum brazing technique directly fuses high-purity synthetic diamonds to steel barrels, eliminating segment shedding, maximizing heat dissipation, and increasing cutting speeds by up to 60%.
From custom laser-etched branding and color-coded depth indicators to localized barcode packaging and customized thread connections (1-1/4"-7 UNC, 1/2 BSP, M14, Hilti end-fittings), we provide turnkey OEM integration.
Dual-warehouse operational model coupled with automated reorder pipelines ensures rapid dispatch, minimizing lead times for high-volume wholesale distributors and machinery rental partners worldwide.
The global construction, demolition, and architectural glass-processing industries demand unprecedented levels of performance, tool longevity, and operator safety. As a leading manufacturer specializing in Custom OEM Core Drill Factories & Factory direct solutions, our engineering philosophy bridges advanced powder metallurgy, automated diamond crystallization matrix synthesis, and precision machine integration.
In modern high-tensile concrete coring and precision surface preparation, standard off-the-shelf diamond tooling frequently fails due to bond thermal degradation, premature diamond stripping, or segment detachment under high shear stress. This technical whitepaper explores the critical engineering parameters, procurement considerations, and metallurgical advancements shaping next-generation OEM core drill bits, vacuum brazed hole saws, and diamond grinding cup wheels.
In field performance testing, our vacuum-brazed core bits achieved an average linear drilling speed of 180 mm/min in 35 MPa reinforced concrete, outperforming conventional silver-welded segmented cores (110 mm/min) while retaining structural diamond density across 100% of the working depth.
The core performance of any diamond drill bit or surface grinding cup wheel relies upon the interaction between the industrial diamond grit and the surrounding metallic bond matrix. In our OEM manufacturing facilities, powder metallurgy is controlled through high-vacuum sintering, hot-isostatic pressing (HIP), and automated furnace atmosphere monitoring.
A common failure mode in low-tier core drill manufacturing is "glazing"—a phenomenon where the metallic matrix fails to wear down at a rate proportional to diamond wear, causing the tool to skid rather than cut. Conversely, if the matrix is too soft, diamonds are prematurely released before utilizing their working crystalline edges.
| Substrate Category | Material Compressive Strength / Abrasiveness | Recommended Matrix Alloy Base | Diamond Grit Selection (MBD/SDB Grade) |
|---|---|---|---|
| Reinforced High-Cured Concrete | > 45 MPa / Non-abrasive, high aggregate hardness | Bronze / Cobalt-Rich Soft Bond | Coated High-Toughness Monocrystalline (40/50 Mesh) |
| Green Concrete & Asphalt | < 20 MPa / Extremely high silica abrasiveness | Tungsten Carbide / Nickel-Iron Hard Bond | Standard Synthetic Diamond (30/40 Mesh) |
| Architectural & Float Glass | Brittle, high-crack propagation sensitivity | Sintered Fine-Grain Copper-Tin Matrix | Micro-Fine Micronized Grit (120/140 Mesh) |
| Epoxy & Polymer Coatings | Viscous, low melting point, high friction heat | Vacuum Brazed Exposed Matrix / Carbide Chip | Coarse Vacuum Brazed Diamond / Carbide Clusters |
When specifying OEM diamond tools, procurement engineers must evaluate the mechanical joining methodology that connects the diamond segment or surface to the tool's steel body (barrel or plate). Our factory utilizes three primary production technologies:
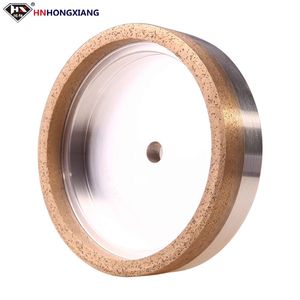
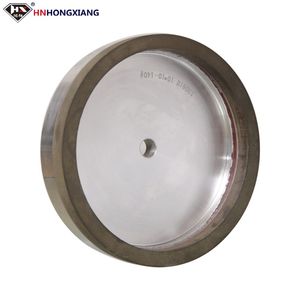
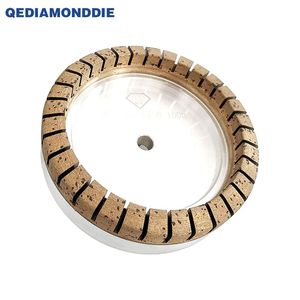
Sintering involves cold pressing metal powders and diamond grit into mold cavities, followed by high-temperature heat treatment. While highly cost-effective for general masonry and glass polishing tools (such as our Full-Toothed Glass Grinding Wheels), sintered segments have mechanical temperature limits. Sintered tools are ideal for wet-use applications where consistent liquid cooling is guaranteed.
For heavy-duty professional core drilling into steel-reinforced structural concrete, laser welding provides exceptional bond strength. A high-energy CO2 or fiber laser melts the steel base of the diamond segment directly to the steel barrel, creating a seamless metallic joint. This eliminates the risk of segment loss due to heat generated during dry drilling operations. All our heavy-duty core bits undergo 100% torque shear testing exceeding EN 13236 safety protocols.
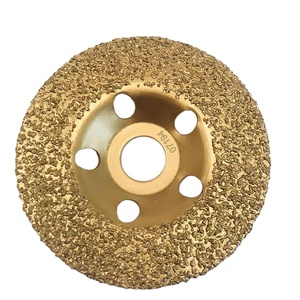
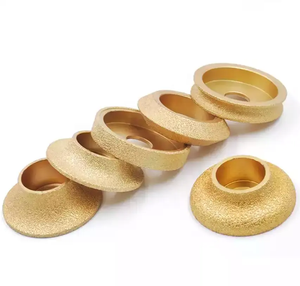
Vacuum brazing represents a paradigm shift in core drill and cup wheel manufacturing. Rather than embedding diamond grains inside a multi-layer metal matrix (where only 15-20% of diamonds are exposed at any time), vacuum brazing uses specialized active braze alloys (nickel-chromium base) in a zero-oxygen vacuum furnace at temperatures exceeding 1,000°C.
As the international construction equipment market evolves, purchasing managers and OEM buyers are adjusting their supply chain criteria. We observe four distinct strategic trends reshaping procurement:
With international regulatory bodies (such as OSHA in the United States and EU-OSHA in Europe) strictly enforcing permissible exposure limits (PEL) for respirable crystalline silica (RCS), contract job sites now require integrated dust extraction tools. Custom OEM core drill manufacturers must design tools featuring integrated internal water feeds, targeted vacuum shrouds, and optimized segment fluting that directs dust slurry immediately into containment systems. Our 10L to 60L battery-powered dust suppression tanks and targeted dry-coring core bits reflect this shift.
Contractors increasingly avoid wet drilling in indoor renovation, electrical retrofit, and high-rise commercial environments due to slurry damage and cleanup costs. Modern OEM core drill factories are investing heavily in dry-coring barrel designs featuring spiral heat sink fluting, thin-wall steel tubing, and laser-welded roof-top segment geometries that maintain stability without liquid coolants.
To reduce inventory complexity, global distributors require modular core bit systems. Instead of stocking separate bit lines for Hilti, Milwaukee, Bosch, and Husqvarna machines, factory-customized OEM threads (such as 1-1/4"-7 UNC female, 1/2" BSP, SDS-Plus, SDS-Max, and Quick-Change hex shanks) combined with precision-machined CNC adapters allow single core bodies to fit diverse power tool fleets seamlessly.
Tier-1 industrial suppliers are auditing factories for carbon footprint, material reusability, and environmental management. Under our ISO 14001:2015 certification, our factories implement steel core recycling programs, non-toxic plating finishes, and 100% recyclable mono-material packaging, allowing OEM partners to fulfill corporate sustainability ESG goals.
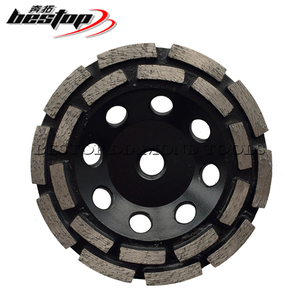
A major differentiator between low-cost regional suppliers and high-tier OEM core drill factories is geometric runout precision and dynamic balancing. Operating a 150mm diamond core bit or 125mm floor grinding cup wheel at 10,000 RPM creates immense centrifugal forces. Minor mass imbalances cause intense vibration, premature hand-arm vibration syndrome (HAVS) in operators, spindle bearing failure in costly power tools, and uneven diamond segment wear.
Every custom OEM batch manufactured in our facility undergoes rigorous Quality Assurance checkpoints:
Our OEM collaboration model is engineered to take private-label concept specifications to mass-market production efficiently:
We evaluate your target market substrate (e.g., green concrete, glass edge polishing, marble slab cutting), machine horsepower, RPM range, and wet/dry operational preferences.
Metallurgical chemists formulate a custom bond powder composition and select synthetic diamond mesh size, crystalline shape, and coating (Ti or Ni coating).
Test batches are produced within 7-10 days using CNC precision machining and high-frequency automated induction or laser welding.
Prototype samples undergo automated robotic drilling and grinding trials to record linear speed, total life (meters/square feet cut), power draw, and dust generation.
Laser etching of customer logo, part numbers, safety icons, and color-matched anodizing/painting are applied alongside custom POS box packaging.
Batch manufacturing under ISO 9001 quality controls with full lot traceability, oSa compliance certification, and scheduled container shipping.
Technical guidance and commercial purchasing questions answered by our engineering and supply chain department.
Partner directly with an audited, ISO-certified core drill and diamond abrasive factory. Request technical specifications, custom OEM pricing, and comprehensive product catalogs today.