Rigorous ISO 9001 and oSa-certified manufacturing standard delivering material-matched performance, high fatigue resistance, and structural longevity across demanding metalworking, stoneworking, and concrete surface preparation applications.
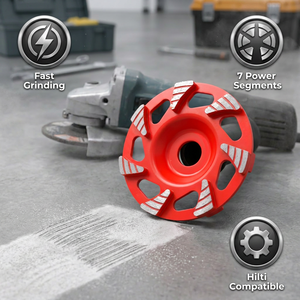
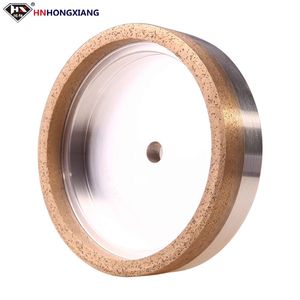
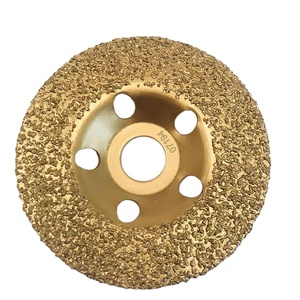
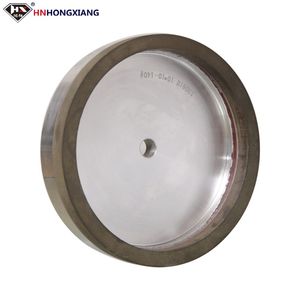
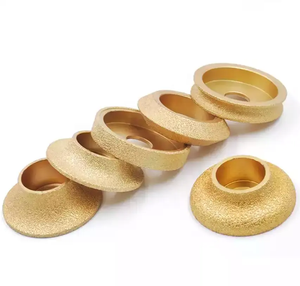
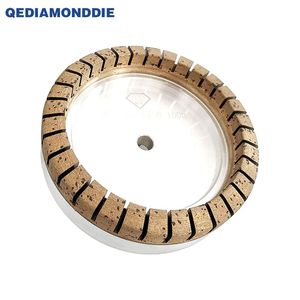
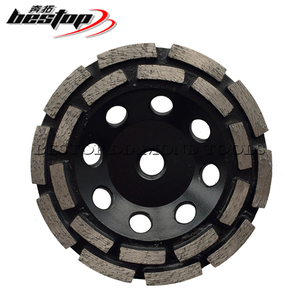
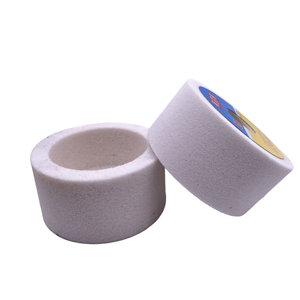
In modern industrial cutting, shaping, and surface processing, high-volume manufacturing facilities and tooling distributors require consumable solutions that go beyond off-the-shelf specs. As a leading Custom OEM Band Saw Manufacturer & Supplier, our engineering division integrates advanced metallurgical science, precise high-frequency tooth setting, and vacuum-brazing diamond technologies to construct industrial cutting systems tailored specifically to client machine specifications and material challenges.
Whether processing structural titanium alloys, reinforced concrete, architectural safety glass, or high-density tool steel, cutting efficiency is governed by three fundamental factors: beam structural stability, tooth micro-geometry, and matrix bond hardness. Our OEM engineering protocol starts with an in-depth substrate analysis to match the blade dynamic properties—minimizing kerf loss, optimizing chip load per tooth, and eliminating premature beam fatigue or segment stripping.
Utilizing high-chrome spring steel backings heat-treated to 44–46 HRC for exceptional beam strength, flex-life fatigue resistance, and high tension stability up to 300 MPa.
High-energy bi-metal joints fusing M42/M51 high-speed steel or micro-grain tungsten carbide tips onto backing bands with zero thermal degradation of the blade body.
Custom sintering and vacuum brazing processes designed for diamond grinding cup wheels, matching segment matrix erosion rates precisely to substrate abrasiveness.
Through our comprehensive OEM manufacturing framework, we offer private-label branding, specialized packaging solutions, localized sizing modifications, and exact TPI (Teeth Per Inch) configuration tailored for automated band saw machines, floor grinders, glass edging equipment, and hand-held power tools.
Maximizing cutting speed while preserving tool life requires precise alignment between the workpiece metallurgy, machine operating metrics, and blade/wheel design parameters. Below is an engineering selection framework established from field testing across automated industrial work sites.
| Substrate Material | Recommended Blade / Tool Type | Ideal Tooth Pitch / Diamond Grit | Linear Speed (m/min or m/s) | Primary Wear Prevention Factor |
|---|---|---|---|---|
| Structural Steels & Inconel | Bi-Metal M51 / Carbide-Tipped Band Saw | 2/3 TPI or 3/4 Variable TPI | 25 – 45 m/min | High thermal resistance, slow speed high torque feed |
| Cured Concrete & Hard Aggregates | 7-Segment Aggressive Diamond Cup Wheel | 30/40 Coarse Diamond Grit | 35 – 45 m/s | Soft metal matrix bond for continuous diamond exposure |
| Architectural Safety Glass | Full-Toothed Sintered Glass Cup Wheel | 120/140 Fine Finishing Grit | 28 – 35 m/s | Ultra-fine concentric tolerance to eliminate micro-chipping |
| Epoxy, Mastic & Elastomeric Coatings | Vacuum Brazed Carbide Cup Wheel | Coarse Vacuum Brazed Chips | 40 – 50 m/s | Wide chip clearance channels preventing heat softening |
| Hardened Tool Steels (>55 HRC) | WA Ceramic Vitrified Grinding Wheel | WA 60-J Vitrified Matrix | 20 – 30 m/s | Self-sharpening ceramic grain fracturing under load |
Proper tensioning and blade coolant delivery play pivotal roles in cutting accuracy. For band saws, maintaining a constant strain parameter between 250 N/mm² and 300 N/mm² prevents lateral deflection (wandering cuts), while suppressing harmonics that cause micro-fracturing on tungsten carbide blade tips.
As global manufacturing demands shift toward elevated precision, reduced energy consumption, and strict workplace safety compliance, the industrial saw blade and diamond abrasive sector is undergoing substantial technological evolution. B2B buyers and supply chain managers must align their procurement strategies with four key emerging industry trends:
Standard bi-metal blades are increasingly being augmented by micro-grain tungsten carbide (WC) formulations enhanced with physical vapor deposition (PVD) titanium aluminum nitride (TiAlN) coatings. In high-speed band sawing operations, these coatings lower friction coefficients by up to 35%, enabling dry-cutting of structural steel while increasing overall band flex-life by over 40%.
Global regulatory frameworks (such as OSHA and EU directives) are heavily penalizing dry-grinding operations that produce respirable crystalline silica (RCS) dust. Procurement teams are heavily favoring integrated dust suppression systems and diamond cup wheels engineered with aerodynamic vacuum extraction vents. OEM manufacturers who provide certified safety tooling—audited under EN 13236 and ISO 14001 environmental standards—are establishing decisive competitive advantages in municipal and civil engineering tenders.
Modern automated band saw machinery now incorporates real-time load sensors that adjust downward force and band velocity based on real-time blade vibration and cutting temperature. This intelligent machining trend requires OEM blade manufacturers to supply blades with extremely consistent thickness tolerances (±0.01mm) and computer-balanced tooth kerfs to prevent false sensor triggers.
In response to global logistics volatility, major distributors and industrial end-users are moving away from multi-tiered sourcing toward single-source OEM partners capable of supplying cross-disciplinary tooling portfolios. Sourcing band saws, diamond core bits, grinding cup wheels, and ceramic abrasives under a consolidated OEM agreement significantly streamlines quality assurance, freight management, and warranty traceability.
With over two decades of dedicated manufacturing experience, DURO Yokota Ltd delivers end-to-end OEM and ODM tooling solutions designed to maximize distributor margins and operational stability for contractors worldwide. Our facilities operate under strict international management systems:
Every band saw body and diamond abrasive product is produced under ISO 9001 quality management, with continuous safety audits meeting EN 13236 and EN 12413 standards to prevent blade rupture or segment detachment.
Certified under ISO 14001, ISO 45001, and ISO 27001, ensuring eco-responsible manufacturing, workplace health and safety compliance, and robust data protection for proprietary OEM customer drawings.
Deep inventory buffers across strategic warehouse hubs enable rapid order dispatch, custom batch production, next-day shipping options, and guaranteed safety stock reserves for corporate buyers.
Our engineering team assists OEM partners through every phase of product development: from micro-grain carbide selection and custom tooth pitch grinding to private-label silk screening, barcode integration, and tailored point-of-sale packaging design.
Direct answers from our engineering and procurement teams addressing common OEM buyer technical inquiries.
TPI selection depends on substrate thickness and cross-section shape. As a general engineering rule, maintain between 3 and 12 teeth inside the cut at all times. Thin-walled tubing requires finer pitch (e.g., 8/12 or 10/14 TPI), whereas large solid billets require coarse pitch (e.g., 2/3 or 1.4/2 TPI) to accommodate chip volume and avoid clogging.
Vacuum brazing fuses diamond or carbide particles directly to the steel body using a high-strength nickel-alloy matrix under high vacuum. This eliminates segment joint loss risk, provides 100% diamond exposure from the first pass, increases removal speeds by up to 60%, and allows aggressive dry-cutting of non-traditional composites, rubber coatings, and glass.
Yes. As a dedicated OEM supplier, we weld band saw blades to exact loop lengths tailored to all major band saw machine brands (e.g., Amada, Behringer, Kasto, DoALL). Similarly, diamond cup wheels and vitrified ceramic wheels can be produced with custom arbor bores (e.g., 22.23mm, 25.4mm, 50mm) or custom drive-pin hole patterns.
All DURO diamond grinding products are produced in oSa® (Organization for the Safety of Abrasives) audited facilities. Manufacturing plants comply strictly with European Safety Norms EN 13236 (for superabrasives) and EN 12413 (for bonded abrasives), backed by ISO 9001 quality management oversight.
Glazing occurs when hard aggregate dulls diamond edges without eroding the surrounding metal matrix. Our metallurgists customize the bond hardness (ranging from soft bronze-cobalt alloys to hardened nickel matrices) to match the abrasive index of the target concrete, ensuring continuous micro-fracturing and exposure of fresh diamond grains.
Standard OEM private label production runs typically start at 100 pieces per specification for diamond cup wheels, or 50 welded loops for industrial band saws. Initial artwork approval and sample validation take 7–10 working days, with batch shipment dispatched in 3–4 weeks via our global distribution network.
Request custom metallurgical specifications, private label branding kits, wholesale volume pricing, or technical data sheets from our engineering division today.
Get Catalog