Engineered for extreme duty on bridge saws, continuous edging machines, and heavy floor grinders. Fully compliant with EN 13236 safety protocols.
An engineering guide for procurement managers, equipment importers, and industrial stone fabrication plant directors searching for audited OEM partners in China.
China’s stone bridge saw and diamond tooling manufacturing sector has evolved from high-volume standardized production into advanced precision engineering. Leading Chinese exporters now integrate computerized hot-press sintering, vacuum brazing, and automated 5-axis CNC laser-welding lines capable of holding runout tolerances under 0.02mm.
When selecting bridge saw blades (spanning 350mm to 3500mm diameters) and associated grinding cup wheels, procurement specialists must evaluate the sinter bond chemistry. The ideal matrix balances cobalt (Co), nickel (Ni), and bronze (Cu-Sn) powder ratios against material hardness—ranging from soft abrasive sandstones to ultra-dense Class 5 engineered quartzites.
Industrial stone cutting operates under extreme rotational velocities (up to 80 m/s peripheral blade speeds). Segment detachment presents severe physical risks. Top-tier Chinese manufacturers undergo rigorous auditing to hold active membership in the oSa® (Organization for the Safety of Abrasives).
Purchasing directors must verify that factory production strictly complies with EN 13236 (Safety requirements for superabrasive products) and EN 12413 for bonded abrasives, supported by comprehensive ISO 9001:2015 Quality Management and ISO 45001:2018 Occupational Health protocols.
Understanding segment matrix formulation ensures optimized cutting linear meters and minimal amperage draw on bridge saw drive motors.
| Matrix Bond Grade | Bond Composition Focus | Target Substrate Hardness | Diamond Grit (US Mesh) | Recommended Cooling |
|---|---|---|---|---|
| Extra Soft (B1) | High Cobalt / Tungsten Matrix | Class 5 Granite, Quartzite, Hard Porcelain | 30/40 or 40/50 Mesh | High-Pressure Water Feed |
| Medium Soft (B2) | Balanced Co-Ni-Cu Sinter | Class 3–4 Granite, Hard Marble, Concrete | 40/50 Mesh | Standard Water Feed |
| Standard (B3) | Bronze-Iron Sintered Bond | Medium Marble, Terrazzo, Slate | 50/60 Mesh | Wet / Controlled Misting |
| Hard / Tough (B4) | High Copper-Iron Alloy Bond | Abrasive Sandstone, Green Concrete, Asphalt | 30/40 Coarse Mesh | Wet or Dry Extraction |
Combining 20+ years of trade expertise, 150+ years of collective team engineering, and fully integrated international logistics hubs.
Our production facilities maintain independently audited certifications for ISO 9001:2015 (Quality), ISO 14001:2015 (Environmental Management), ISO 45001:2018 (Occupational Safety), and ISO 27001 (Data Security). Every batch of diamond segment is traceable from raw powder synthesis to final blade balancing.
With strategic warehousing hubs maintaining over 40% stock depth dedicated to fast-moving SKUs (including DDC-RAPIDE vacuum brazed cores and bridge saw silent-core blades), distributors benefit from rapid dispatch and reduced transit capital lockup.
We provide four distinct performance tiers—from contractor grade to high-speed industrial processing—allowing procurement teams to match cutting costs per meter directly against job budget and machine horsepower specifications.
Strategic technology shifts every machinery distributor and stone fabrication factory director must account for in their 5-year purchasing strategy.
Modern stone fabrication facilities are rapidly replacing manual monoblock saws with automated 5-axis CNC bridge saws. Tooling must support multi-directional interpolations, miter cutting, and complex sink cutout milling without side-load segment flex.
Suppliers must supply high-concentricity core bodies with dynamic rotational balance tolerances under 0.15 grams/cm to prevent high-speed spindle bearing wear.
Global regulatory agencies (including OSHA in the US and HSE in Europe) have instituted strict limits on Respirable Crystalline Silica (RCS). Sourcing trends heavily favor integrated wet-feed bridge tooling and specialized dust suppression water tanks (ranging from 10L to 60L battery-powered mobile units).
Tooling designs that reduce micro-dust atomization while maintaining thermal dissipation are capturing premium market share.
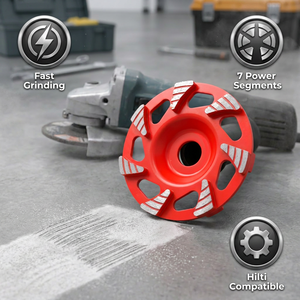
While sintered diamond segments remain the standard for deep bridge saw blades, Vacuum Brazing (VB) has taken over cup wheels, core drills, and profile wheels. VB technology fuses synthetic diamond crystals directly to the steel substrate with a nickel-braze alloy.
This delivers 100% diamond exposure, offering up to 60% faster material removal rates without segment stripping risks during aggressive coating removal.
How state-of-the-art Chinese exporters are achieving superior blade lifespan and noise dampening through physical metallurgy.
Urban acoustic regulations have driven major advancements in bridge saw blade steel cores. Modern high-performance blades incorporate a sandwich steel-copper-steel core configuration.
A thin copper foil dampener is laser-welded between two outer hardened spring-steel layers. This absorbs operational harmonics, reducing operating noise levels by 8 dB to 15 dB while preventing high-frequency metal fatigue during continuous 24/7 fabrication shifts.
Random diamond distribution in traditional sintered segments often leads to uneven wear and premature drop-out of unspent grit. Advanced 3D array placement positions synthetic diamonds in precise geometric grids throughout the metal matrix.
Every diamond crystal is spaced to receive uniform cooling and chip clearance. This structured arrangement improves cutting velocity by 35% while extending total blade wear life by up to 50% compared to conventional random-sintered alternatives.
Access technical drawing files, flange compatibility tables, speed charts, and factory-direct container pricing for wholesale importers.
Get CatalogIn-depth technical answers addressing blade selection, machine alignment, safety compliance, and OEM private-labeling.
Matching bond hardness is inverse to substrate hardness. Soft, abrasive materials like sandstone, green concrete, or asphalt require a hard, wear-resistant metal bond (high copper/iron) to prevent premature matrix erosion. Conversely, extremely hard materials like quartzite or Class 5 granite require a soft, free-cutting matrix (high cobalt/nickel) that wears away cleanly to continually expose fresh sharp diamond points.
For standard granite cutting, peripheral blade speeds should range between 25 m/s to 35 m/s (approx. 1400–1900 RPM for a 350mm blade). For marble, peripheral speeds can increase to 35–45 m/s. Feed rates depend on motor power and slab thickness; typical pass depths range from 20mm to 50mm per pass at linear travel rates of 1.5 to 4.0 meters per minute.
oSa® (Organization for the Safety of Abrasives) certification guarantees that the manufacturing plant undergoes independent third-party audits verifying compliance with strict European safety standard EN 13236. This includes destructive burst testing, segment shear strength testing, and side-load stress testing, protecting importers from liability risks associated with blade failure or segment detachment.
Silver brazing attaches pre-sintered metal segments onto a steel body using a silver-solder interface. It is ideal for heavy concrete grinding where thick segments provide deep wear depth. Vacuum brazing fuses diamond particles directly to the steel plate in a vacuum furnace using a specialized nickel alloy matrix. Vacuum brazing provides maximum chip clearance, aggressive initial cut, and zero risk of segment detachment during edge work or epoxy stripping.
Water-feed dust suppression at the cutting interface remains the primary engineering control recommended by safety boards worldwide. Continuous water delivery flushes slurry, suppresses airborne dust particles, and cools the diamond segment. For dry grinding applications, tools must be paired with shroud-enclosed continuous rim cup wheels connected to M-Class or H-Class industrial dust extractors equipped with HEPA filtration.
Yes. Established manufacturers provide comprehensive OEM/ODM services, including custom laser engraving on core bodies (logo, part numbers, directional arrows), custom color powder-coating, localized retail box packaging, and custom arbor bore sizing (e.g., 50mm, 60mm, 25.4mm, or customized pin-hole arrangements for specific Italian or German bridge saw spindles).
Elevate your tooling portfolio with industrial-grade bridge saw blades, vacuum-brazed cup wheels, and silica-controlled surface prep equipment. Backed by quad-ISO accreditation, oSa® safety standards, and global logistics capability.