In modern civil construction, surface preparation, and heavy-duty demolition, the demand for precise shank tolerance, impact energy transfer, and cutter geometry has never been higher. Sourcing directly from top-tier Chinese factories requires an in-depth understanding of metallurgical composition, automated vacuum brazing, and international safety compliance.
Selecting a high-performance supplier for SDS Plus, SDS Max hammer drill bits, and diamond grinding cup wheels involves analyzing raw material integrity beyond standard catalogue claims. Industrial testing reveals that premature bit failure in reinforced concrete (rebars) usually stems from substandard cobalt-binder carbide grades or manual silver soldering techniques.
As an established manufacturing entity operating under rigorous quality controls, our enterprise integrates micro-grain tungsten carbide tips (YG8C / YG11C grades) with fully automated high-frequency induction brazing and vacuum heat treatment. This whitepaper serves as a procurement guide for tool importers, industrial distributors, and hire fleets seeking continuous penetration speed, minimal machine fatigue, and complete silica dust compliance.
Explore our top-tier OEM/ODM product lines engineered for heavy concrete, architectural glass, stone, and composite surface prep.
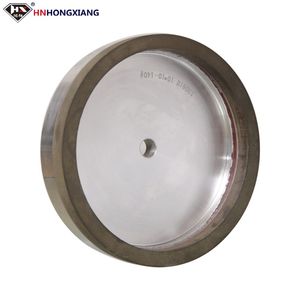
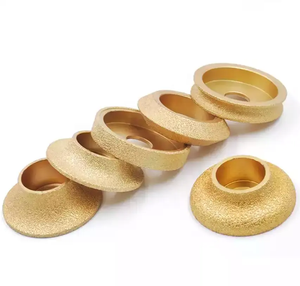
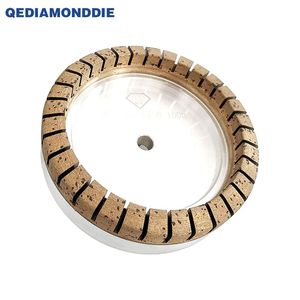
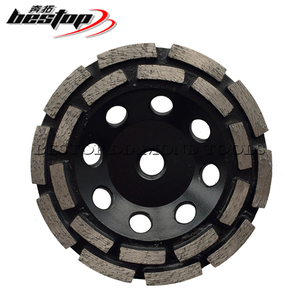
Understanding the raw material engineering, shank machining, and tip-brazing chemistry behind top-tier Chinese manufacturing.
The performance of an SDS Plus or SDS Max bit hinges entirely on the quality of its carbide tip. High-grade Chinese manufacturers utilize ultrafine micro-grain WC-Co alloy powder (90-92% Tungsten Carbide, 8-10% Cobalt).
Unlike standard 2-cutter chisel tips that jam when encountering rebar, specialized 4-cutter solid carbide head geometries feature dynamic centering points. This design pulverizes concrete aggregate evenly and prevents lateral head breakout upon rebar impact.
SDS shanks require strict dimensional tolerance matching ISO/DIN standards (DIN 8035) to prevent energy loss and chunking inside hammer chucks. Modern factories use multi-axis CNC cold milling to create precise drive grooves.
Subsequent controlled salt-bath heat treatment or vacuum quenching creates a gradient hardness: an ultra-hard carbide-brazed head (HRC 88-90), a fracture-resistant core, and a tempered shank (HRC 48-52) capable of absorbing continuous kinetic shocks.
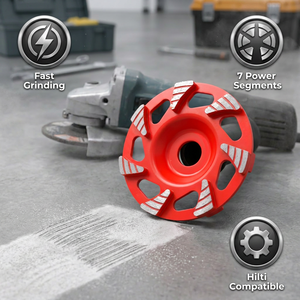
For diamond surface prep tools such as cup wheels and vacuum brazed carbide wheels, segment loss poses a severe safety hazard. Premium manufacturing facilities replace manual flame welding with high-frequency vacuum furnace brazing.
By introducing active nickel-titanium alloy solder, chemical bond strength between diamond crystals and steel backing plates increases exponentially. This allows aggressive 7-segment and double-row cup wheels to run at peripheral speeds up to 80 m/s without thermal shear.
Use the data visualization matrix below to evaluate Chinese SDS bit manufacturers and surface preparation vendors during factory audits:
| Quality Benchmark | Standard Commercial Sourcing | Tier-1 Certified OEM / DURO Standard | Contractor Impact |
|---|---|---|---|
| Carbide Tip Grade | Recycled Scrap WC / YG6 (Low Co) | Virgin Micro-Grain YG8C / YG11C | +300% longer drilling life in C40+ concrete |
| Brazing Shear Strength | Manual Copper Brazing (< 180 MPa) | Vacuum Active Silver-Nickel (> 320 MPa) | Zero segment detachment; safer high-RPM grinding |
| Shank Tolerance (TIR) | > 0.35 mm Total Indicated Runout | ≤ 0.12 mm Precision Ground Shank | Extends hammer drill gear hub & chuck lifespan |
| Dynamic Balancing | Unbalanced / Random Milling | Dynamic Balancing to ISO G6.3 Standard | Minimal hand-arm vibration (HAVS compliance) |
| Dust Control Tech | Dry Only / No Internal Water Channel | Integrated Water Feed / Vacuum Vacuum Ready | Meets OSHA silica dust standards (Respirable Crystalline Silica) |
Strategic technological shifts transforming Chinese factories and global power tool accessory supply chains.
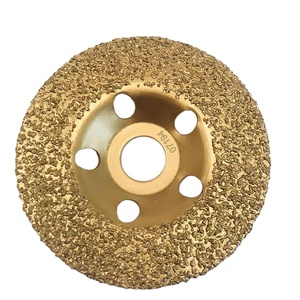
Traditional bonded abrasive wheels are increasingly replaced by vacuum brazed tungsten carbide cup wheels for elastomeric coating, mastic, and epoxy removal. Unlike bonded wheels that load and melt adhesives, vacuum brazed grit cuts cleanly without loading, offering up to 100x the service life.
With strict workplace safety rules regarding respirable crystalline silica (RCS), procurement managers are favoring manufacturers providing integrated dust extraction shrouds, hollow-core SDS drill bits with internal suction channels, and battery-powered dust suppression water tanks.
Leading Chinese OEMs have invested heavily in 6-axis robotic arm welding and visual inspection systems. Automated thermal imaging verifies every brazed joint in real time, eliminating human error in solder volume and ensuring batch-to-batch consistency for OEM private label buyers.
Backing every single piece of tooling we supply is over 150 years of combined team engineering experience and more than 20 years of direct field service to professional construction trades worldwide.
Unlike trading intermediaries, our manufacturing ecosystem operates under quadruply audited ISO management certifications: ISO 9001:2015 (Quality Management), ISO 14001:2015 (Environmental Management), ISO 45001:2018 (Occupational Health & Safety), and ISO 27001 (Information Security).
Direct technical answers from our engineering team regarding procurement, factory customization, and substrate performance.
Sintered cup wheels feature diamond grains fully embedded within a metallic matrix bond, requiring controlled erosion to expose fresh diamond edges. Vacuum-brazed cup wheels bond diamond or tungsten carbide particles directly to the wheel exterior using specialized brazing alloys.
This exposes up to 70% of the crystal surface, providing significantly higher cutting aggressiveness and preventing clogging when removing soft, gummy materials like paint, epoxy, tar, and waterproofing membranes.
Shank breakage typically stems from uneven heat treatment (causing excessive brittleness) or severe runout (TIR) that induces bending stress inside the rotary hammer chuck. Premium Chinese factories mitigate this through dual-stage induction hardening—keeping the shank tough yet flexible (HRC 48-52) while hardening the flute edges.
Furthermore, CNC flute milling guarantees concentricity, preventing bending torque during rebar strikes.
Yes. We support complete OEM/ODM customized manufacturing for global distributors and brand owners. This includes laser engraving part numbers and logos onto bit shanks, custom color powder-coating on diamond grinding cup wheels, customized blister card packing, and color-coded box sleeves tailored to your brand identity.
Every diamond grinding wheel undergoes automated dynamic spin balancing after segment attachment. Micro-amounts of material are precision-milled from the rear steel body shoulder until vibration tolerances fall within ISO G6.3 limits.
This minimizes operator arm-hand vibration (HAVS) and protects angle grinder bearings from premature destruction.
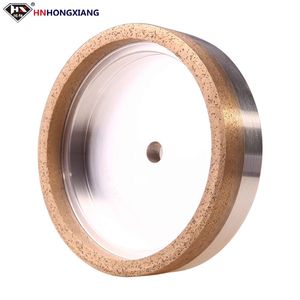
Glass grinding wheels require continuous, uniform water cooling feed to prevent localized thermal cracking of architectural glass. They operate optimal peripheral speeds between 25 m/s and 35 m/s. Sintered continuous rim designs should be used for rough edging, followed by full-toothed or fine-grit resin-bonded wheels for edge polishing.
Importers should demand proof of oSa® (Organization for the Safety of Abrasives) auditing or explicit compliance with European safety standards EN 13236 (for superabrasives) and EN 12413 (for bonded abrasives). Additionally, verifying ISO 9001 quality systems ensures repeatable batch-to-batch metallurgical control.
Partner with an ISO 9001 / 14001 / 45001 / 27001 certified Chinese manufacturer. We offer comprehensive wholesale pricing, custom OEM tooling designs, and rapid global export logistics.