Engineered for extreme material removal rates, substrate longevity, and structural safety across concrete, stone, architectural glass, and metal alloy processing.
Empowering industrial distributors and OEM partners with verified quality standards and deep inventory buffers.
An authoritative technical evaluation of synthetic diamond matrix sintering, vacuum brazing, and vitrified bonding for B2B procurement managers.
Selecting the optimal sanding disc or diamond cup wheel requires an understanding of mechanical wear mechanics. The fundamental rule of diamond tool engineering is inverse bond hardness matching: soft abrasive substrates require hard metallic bonds, whereas hard, dense materials demand soft metal matrices.
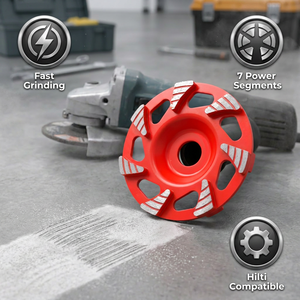
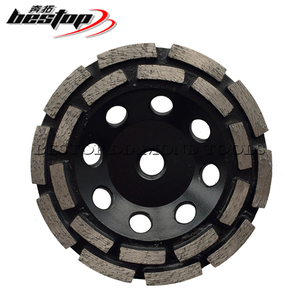
Our manufacturing facility utilizes controlled sintering furnaces under vacuum nitrogen purges to bind cobalt, bronze, iron, and tungsten powders. For floor prep professionals, utilizing a 7-segment aggressive cup wheel (such as Hilti-compatible SUMO models) guarantees maximum contact pressure with optimized dust extraction geometry.
While traditional sintered diamond cup wheels dominate general masonry and concrete grinding, direct-to-substrate monolayer technologies—specifically vacuum brazing—represent a technological leap for sticky, elastomeric coatings.
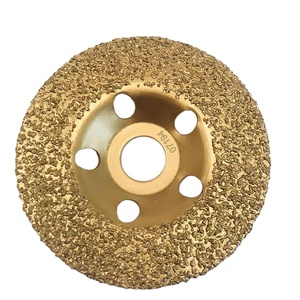
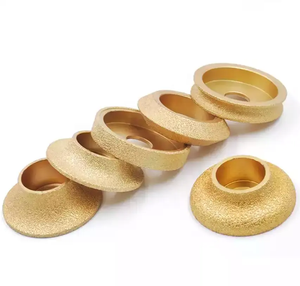
Vacuum brazed tungsten carbide and coarse synthetic diamond cup wheels do not rely on matrix wear to expose abrasive grains. High-temperature nickel-chromium brazing alloys bond diamonds directly to the steel core at the molecular level, creating open clearance channels. This completely prevents gumming, melting, and loading when stripping epoxy coatings, polyurethane membrane, or carpet adhesive.
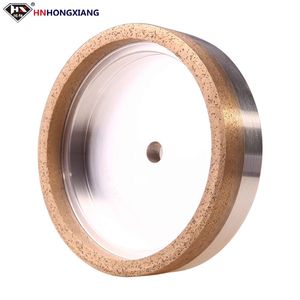
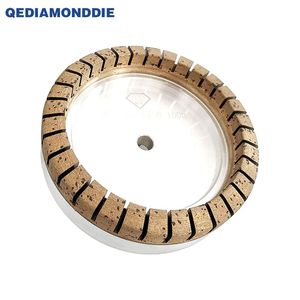
Sanding and grinding discs designed for flat glass, beveling machines, and double-sided edging systems operate under strict hydrodynamic cooling conditions. Full-toothed continuous-rim sintered diamond glass cup wheels utilize micro-grit diamond sizing (ranging from D46 down to D15) suspended in custom bronze-tin matrices.
By balancing segment tooth geometry with coolant flow vectors, our glass grinding cup wheels reduce peripheral edge stress, extending glass tempered safety performance in structural building envelopes.
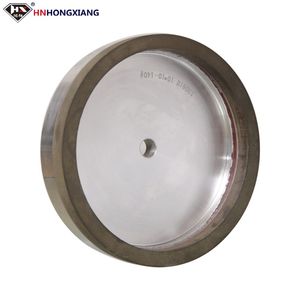
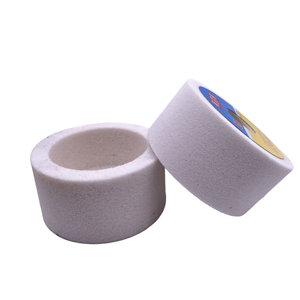
Non-diamond abrasive applications—such as grinding high-speed tool steels, hardened alloy components, and delicate metal knife edges—require high-purity White Corundum (WA). Cup-shaped ceramic vitrified wheels feature friable aluminum oxide grains that fracture cleanly under heat, continuous fresh sharp grain exposure without thermal burning.
Vitrified ceramic bonds deliver extreme structural rigidity, maintaining shape profile during precision tool room room resharpening and heavy stock removal on manual or CNC surface grinders.
Strategic insights for procurement directors preparing supply chains for regulatory compliance and automated surface prep technologies.
Regulatory authorities globally (OSHA in the US, EU-OSHA directives, UK HSE) are enforcing strict Exposure Action Limits for airborne Silica dust. Procurement strategies must align with tooling that features integrated extraction channels and water suppression shrouds.
Future sanding discs and concrete cup grinding wheels are moving toward aerodynamic flow-hole design, channeling fine particulates directly into vacuum cowlings, cutting operator exposure while increasing tool lifespan by reducing heat entrapment.
The transition toward autonomous floor grinding robots and multi-axis glass edge processing machines requires unprecedented consistency in abrasive wheel height, mass distribution, and wear progression.
Supply chain managers are demanding automated dynamic balance testing certificates for every batch, reducing machine spindle bearing fatigue and eliminating chatter marks on automated production lines.
Industrial users are shifting from high-wear resin bonded sandpapers toward multi-use vacuum brazed tungsten carbide and diamond discs. While the initial acquisition cost per unit is higher, the total cost per square meter (m²) drops by up to 45% due to labor downtime reduction and extended service life.
Global buyers now require suppliers to demonstrate sustainable manufacturing practices. This includes closed-loop water filtration during diamond sintering, eco-friendly recyclable packaging, and ISO 14001 Environmental Management verification across the tier-1 manufacturing ecosystem.
Combining 20+ years of industrial field experience with rigorous international quality standards.
All diamond consumables are produced in oSa (Organization for the Safety of Abrasives) audited facilities, fully compliant with EN 13236 and EN 12413 safety parameters.
Operates under audited management systems: ISO 9001 (Quality), ISO 14001 (Environmental), ISO 45001 (Occupational Health & Safety), and ISO 27001 (Information Security).
Allows wholesale distributors to match blade and disc cost directly against client budget and expected cutting/grinding meters, optimizing inventory turnover.
Two centralized automated warehouses maintain high safety stock depth across standard 115mm, 125mm, 180mm, and custom CNC arbor sizes, facilitating quick dispatch.
Direct technical support from onsite metallurgists to evaluate customer substrate samples (concrete PSI rating, glass hardness, coating viscosity) before mass production.
Complete custom branding solutions including specialized laser etching, color-coded cup wheel bodies, customized point-of-sale packaging, and display merchandising.
Partner with China's leading diamond grinding cup wheel and sanding disc manufacturer. Dedicated technical support and factory-direct volume pricing.
Get a QuoteExpert answers to common specification, safety, and sourcing questions for commercial diamond grinding and sanding tools.
Selection depends on machine horsepower, target profile, and removal aggressiveness. 7-Segment Aggressive Cup Wheels (such as SUMO Hilti-compatible models) concentrate machine down-force on fewer, larger segments, allowing deeper penetration into hard concrete and fast leveling of high spots. Double-Row Silver Welded Cup Wheels distribute weight over 16–20 segments, delivering a smoother scratch pattern ideal for fine finishing before sealing or applying thin coatings.
Epoxy, thick urethane coatings, and elastomeric membranes melt under frictional heat generated by standard diamond grinding wheels. The melted material smears across diamond segments, clogging matrix pores ("loading" or "glazing"). Vacuum brazed tungsten carbide cup wheels feature wide open matrix structures with sharp carbide edges that chip and shear elastic coatings off the substrate without heat buildup, completely eliminating disc clogging.
Procurement teams must ensure suppliers hold **oSa (Organization for the Safety of Abrasives)** certification and comply with European Safety Standards **EN 13236** (for superabrasives like diamond/CBN) and **EN 12413** (for bonded abrasives like White Corundum). These certifications mandate rigorous destructive testing, including segment shear strength testing and burst speed safety factors up to 1.5x maximum operating RPM.
Glass grinding cup wheels utilize micro-grained synthetic monocrystalline diamonds suspended in a bronze-tin metal sintered matrix. They require continuous water delivery to prevent thermal shock micro-cracks in glass sheets. Full-toothed segment design ensures smooth, vibration-free edge grinding on straight-line edgers and double-sided machines, leaving clean pencil edges or flat bevels ready for tempering.
This follows the inverse matching rule: Soft, abrasive concrete quickly erodes standard metal matrix bonds, releasing diamonds prematurely and causing rapid wheel wear. Soft concrete requires a **hard bond matrix** (reinforced with tungsten powder). Conversely, hard concrete (high PSI or quartz aggregate) resists wear, which can dull diamonds; hard concrete requires a **soft bond matrix** that wears away predictable layers to continually expose fresh, sharp diamond edges.
We provide comprehensive OEM manufacturing including non-standard arbor bore sizes (e.g., 22.23mm, 5/8"-11 threaded flanges, Hilti quick-lock bases), custom body powder-coating colors, private label laser etching on steel cores, custom dynamic balancing tolerances, and tailor-made retail display boxes to support distributor brand identity.
The most effective controls involve engineering the tool and shroud interface. Our diamond grinding cup wheels are designed with optimized airflow vent holes that line up with standard vacuum dust shrouds (H-Class dust extractors). For dry coring and grinding, combining high-flow extraction shrouds with continuous segment airflow keeps airborne respirable crystalline silica (RCS) well below OSHA Permissible Exposure Limits (PEL).
Standard stocked lines across standard sizes (115mm to 180mm) ship within 3 to 5 business days. Custom OEM production runs (including specialized segment formulations or custom steel cores) typically feature a manufacturing cycle of 15 to 25 days, supported by complete ISO 9001 quality inspection reports prior to ocean or air freight loading.
Have specific project requirements or looking for verified factory-direct pricing? Our application specialists are available 24/7.
Get a Quote