Engineered to oSa® and EN 13236 standards for high-speed concrete floor preparation, glass edge finishing, masonry drilling, and metal processing.
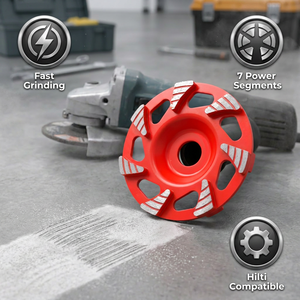
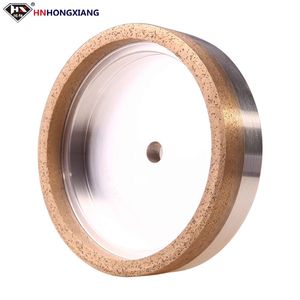
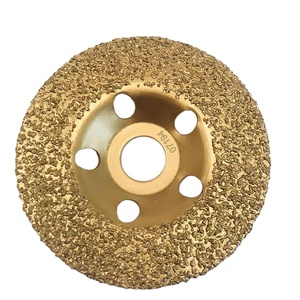
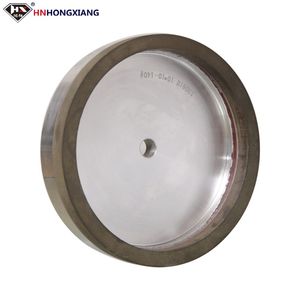
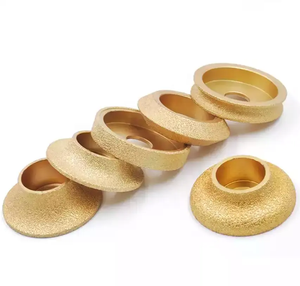
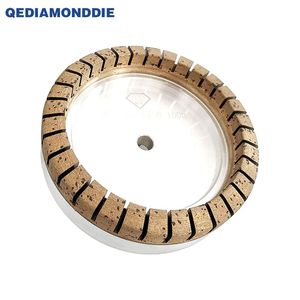
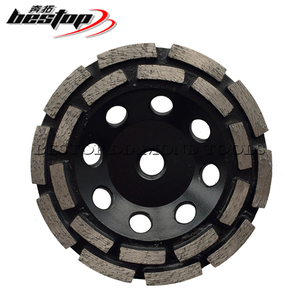
As a global OEM/ODM manufacturer and exporter of heavy-duty power tool accessories, our core operations adhere to internationally audited management frameworks. Every drill bit, vacuum brazed core barrel, and diamond grinding cup is produced in facility ecosystems fully certified under ISO 9001:2015 (Quality Management), ISO 14001:2015 (Environmental Management), ISO 45001:2018 (Occupational Health & Safety), and ISO 27001 (Information Security).
Our strict adherence to the European safety standard EN 13236 for superabrasive products ensures maximum shear strength at segment joints, eliminating segment detachment under intense torque and thermal loads.
Theoretical calculations cannot substitute live job-site validation. Our engineering testing protocol subjects every new matrix bond, shank geometry, and diamond grit formulation to real-world substrate resistance trials across heavily reinforced concrete (rebar C50/60+), natural granite, hard engineering brick, and abrasive asphalt.
By controlling raw material inputs—using premium synthetic diamond crystals coated with titanium/nickel jackets—we deliver repeatable cutting linear meters and consistent drill hole geometry for anchor installation security.
A technical analysis of joint mechanics, segment geometry, and substrate friction engineering in modern hole-making consumables.
Unlike conventional sintering where diamond grit is embedded deep inside a metallic powder matrix, high-temperature vacuum brazing (using active alloy brazing filler materials like Ti-Cr-Ni) chemically bonds mono-crystalline diamond particles directly to the tool's structural steel body. This creates a monolayer exposure reaching up to 70-80% of particle height without matrix loss, guaranteeing 60% faster drilling speeds and zero risk of segment detachment during severe torsional impacts.
For deep core drilling rigs operating under high water pressure and extreme thermal expansion, automated multi-axis laser beam welding creates an intermetallic fusion zone between the diamond segment base and the steel barrel. Tensile strength tests confirm laser welds exceed 850 MPa shear stress thresholds, outperforming traditional silver-soldered joints by over 300% under dry drilling thermal peaks (>600°C).
Optimizing linear meter tool life requires fine-tuning diamond grit concentration (ranging from 20% to 45% volume) and mesh sizing (from coarse 20/30 mesh for soft abrasive asphalt to 40/50 fine mesh for dense granite). Soft metal bonds (cobalt-bronze matrices) wear continuously to expose fresh diamonds when tackling hard materials, while hard bonds (tungsten carbide-iron matrices) resist wear when drilling highly abrasive green concrete.
| Manufacturing Technology | Bond / Matrix Type | Primary Target Substrates | Thermal Threshold (°C) | Relative Cutting Velocity | Risk of Joint Failure |
|---|---|---|---|---|---|
| Vacuum Brazing (e.g. RAPIDE Series) | Active Titanium-Nickel Alloy Monolayer | Porcelain, Granite, Reinforced Concrete, Steel Tube | 850°C | Fastest (+60% vs Sintered) | Negligible (Chemical Bond) |
| Automated Laser Welding | Cobalt-Iron Powder Sintered Segment | C30-C80 Concrete, Hard Engineering Brick | 600°C (Dry Operation) | High Velocity | Extremely Low (>850 MPa Shear) |
| High-Frequency Silver Brazing | Silver-Copper Flux Solder Base | Wet Core Drilling in Masonry & Light Concrete | 350°C (Requires Water Flow) | Standard High Speed | Medium if Water Feed Fails |
| Cold Press / Hot Press Sintering | Bronze-Iron Matrix Consolidation | General Masonry, Tiles, Glass Edge Polishing | 400°C | Moderate Speed | Integrated Segment Body |
Strategic shift markers shaping commercial tool procurement, environmental directives, and job-site safety standards worldwide.
Global regulatory enforcement by OSHA (29 CFR 1926.1153 in the US) and the EU Directive 2017/2398 has mandated integrated engineering dust controls. Future purchasing trends indicate a decisive shift away from unassisted dry cutting toward battery-powered mobile dust suppression water feed tanks (10L–60L capacity) and core bits designed with optimized internal vacuum airflow channels.
Tool buyers require suppliers who supply certified closed-loop wet drilling assemblies to keep airborne silica concentrations below the permissible exposure limit (PEL) of 0.05 mg/m³ over an 8-hour time-weighted average.
As 18V, 36V, and high-voltage battery equipment replaces corded job-site machines, drill bit and blade designs are undergoing thin-kerf re-engineering. By narrowing segment width by 15-25%, cutting friction torque is significantly reduced.
This allows cordless hammer drills and core motors to yield up to 35% more holes per battery charge while protecting internal brushless motors from thermal overload shut-offs during high-depth anchor drilling in reinforced concrete.
Tier-1 tool distributors and industrial brand managers are shifting procurement toward factories providing complete end-to-end OEM customization. Beyond custom laser-etched branding and color-coded performance tiers (e.g., Speed, Life, Universal, Premium), procurement specifications now demand full batch metallurgical traceability.
In accordance with ISO 27001 data integrity standards, enterprise buyers expect digitally verified batch certificates detailing diamond origin, steel shank hardness (HRC rating), and dynamic balance testing logs.
To reduce fleet inventory costs, contractors prefer multi-compatible fitment systems. Our factory lines support universal shanks across SDS-Plus, SDS-Max, 1-1/4" UNC female, 1/2" BSP male, M14 thread, and custom quick-release hex systems compatible with Hilti, Bosch, Makita, DeWalt, and Milwaukee machinery platforms.
Smart procurement managers evaluate drill bits and abrasive wheels based on Cost Per Hole / Meter Cut rather than initial purchase price alone. Low-cost uncertified bits suffer from rapid diamond stripping, segment breakage, and high heat generation, causing extensive worker labor downtime during frequent bit replacements.
By engineering high-density diamond matrices and precision vacuum brazing, our CE certified bits maintain a steady penetration velocity from the 1st hole to the 500th hole. This stability minimizes labor overheads and prevents motor armature burnout on high-value power tools.
Direct answers from our application engineering department regarding certification, material pairing, and global logistics.
Our diamond tools undergo rigorous destructive and non-destructive testing prior to export. To comply with EN 13236 and CE directives, products are subjected to centrifugal burst-speed testing at 1.5 times the maximum operational RPM, side-load bending tests to verify weld integrity, and automated shear force testing ensuring laser-welded and brazed joints exceed 850 MPa resistance before batch approval.
In audited site trials using identical power heads, vacuum brazed core bits (such as our RAPIDE series) achieved up to 60% faster penetration speed in reinforced concrete and masonry. Because the synthetic diamond matrix is chemically bonded with 70% exposed edge height—rather than sunken inside sintered metal powder—friction heat is drastically minimized, maintaining maximum cutting aggression without glazing over.
The inverse rule of diamond tooling applies: hard substrates require a soft metal bond, while soft, abrasive substrates require a hard metal bond. Soft, highly abrasive materials (like green concrete, asphalt, or sandstone) wear away tooling rapidly; thus, a hard bond matrix (tungsten-iron base) is required to retain diamond grit. Conversely, hard, dense substrates (such as granite, engineering brick, or C60 rebar concrete) require a soft bond matrix (cobalt-bronze base) that erodes steadily to expose sharp new diamonds continuously.
We supply a complete dust suppression ecosystem. For wet drilling and cutting, we manufacture heavy-duty 10L to 60L dust suppression water tanks (including 20L and 60L 18V battery-powered automatic pressure tanks). For dry cutting, our tool cowlings and diamond blades are engineered with aerodynamically placed segment gullets designed to channel dust directly into connected M-Class or H-Class industrial extraction vacuums, fully complying with OSHA silica exposure regulations.
Yes. We provide complete OEM/ODM production services for global brand owners, wholesale distributors, and equipment rental fleets. Services include custom shank machining (SDS, UNC, BSP, Hex, Threaded), private label laser engraving, bespoke color powder coating, localized packaging design, and full logistical documentation support for ocean, air, and express freight delivery worldwide.
From individual wholesale stockist programs to high-volume custom OEM manufacturing, our enterprise infrastructure delivers certified performance, stable inventory reserves, and dedicated technical application support.